



 +86 18920794106
Leave Your Message
-
Contact WhatsApp
-
 Contact Phone
-
 Contact Email
Explore our high-tensile, heavy-duty rubber conveyor belts engineered to withstand the demanding operational environments of Greater London's key industrial hubs.
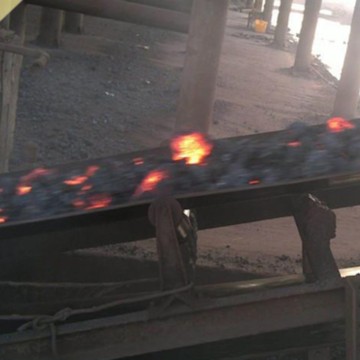
Engineered for London's asphalt, metallurgy, and high-temp processing plants.
Learn More
Meets strict UK safety standards for underground tunneling and mining operations.
Learn More
Designed for outdoor winter operations and cold storage logistics in the UK.
Learn More
Ideal for high-elevation vertical transport in London's construction sites.
Learn MoreLondon is globally recognized as a financial powerhouse, but behind its iconic skyline lies a massive, highly sophisticated industrial and logistical infrastructure. From the bustling logistics corridors along the M25 and the Thames Gateway to major recycling, waste management, and infrastructure expansion projects like the Thames Tideway and railway upgrades, the demand for heavy-duty material handling systems is at an all-time high. At the heart of these systems are industrial rubber belts—vital components that keep London’s supply chains, construction projects, and recycling plants moving 24/7.
As a leading rubber belts factory and manufacturer catering to the London market, we specialize in high-tensile, durable, and highly efficient belting solutions. London’s strict regulatory framework regarding safety, environmental sustainability, and operational noise demands products that are not only robust but also compliant with UK and European standards. Our advanced manufacturing processes ensure that every belt delivered to London is optimized for low energy consumption, minimal downtime, and long service life under heavy load conditions.
Engineered to transport aggregates, concrete, and construction waste across London's massive urban development sites.
Tailored for safety-critical environments like London's underground transit networks and recycling facilities.
Optimized compounds that reduce friction, lowering the overall carbon footprint of London's automated logistics hubs.
1. Waste Management & Circular Economy: London is leading the way in waste-to-energy and recycling initiatives. Facilities along the River Thames rely heavily on our abrasion-resistant and general-purpose rubber conveyor belts to sort, transport, and process municipal solid waste, metals, and plastics. The high durability of our belts prevents punctures and tears from sharp scrap materials, ensuring continuous operation.
2. Aggregates and Infrastructure: With major infrastructure upgrades constantly underway, handling bulk aggregates, sand, and gravel is a key requirement. Our nylon-rubber and polyamide (NN) conveyor belts provide the high elasticity and impact resistance needed at London's concrete batching plants and rail freight depots.
3. Port & Terminal Logistics: The Port of London and various Thames-side wharves process millions of tonnes of cargo annually. High-capacity rubber lifting belts and general-purpose belts facilitate the rapid loading and unloading of bulk vessels, maintaining London's connection to global trade.
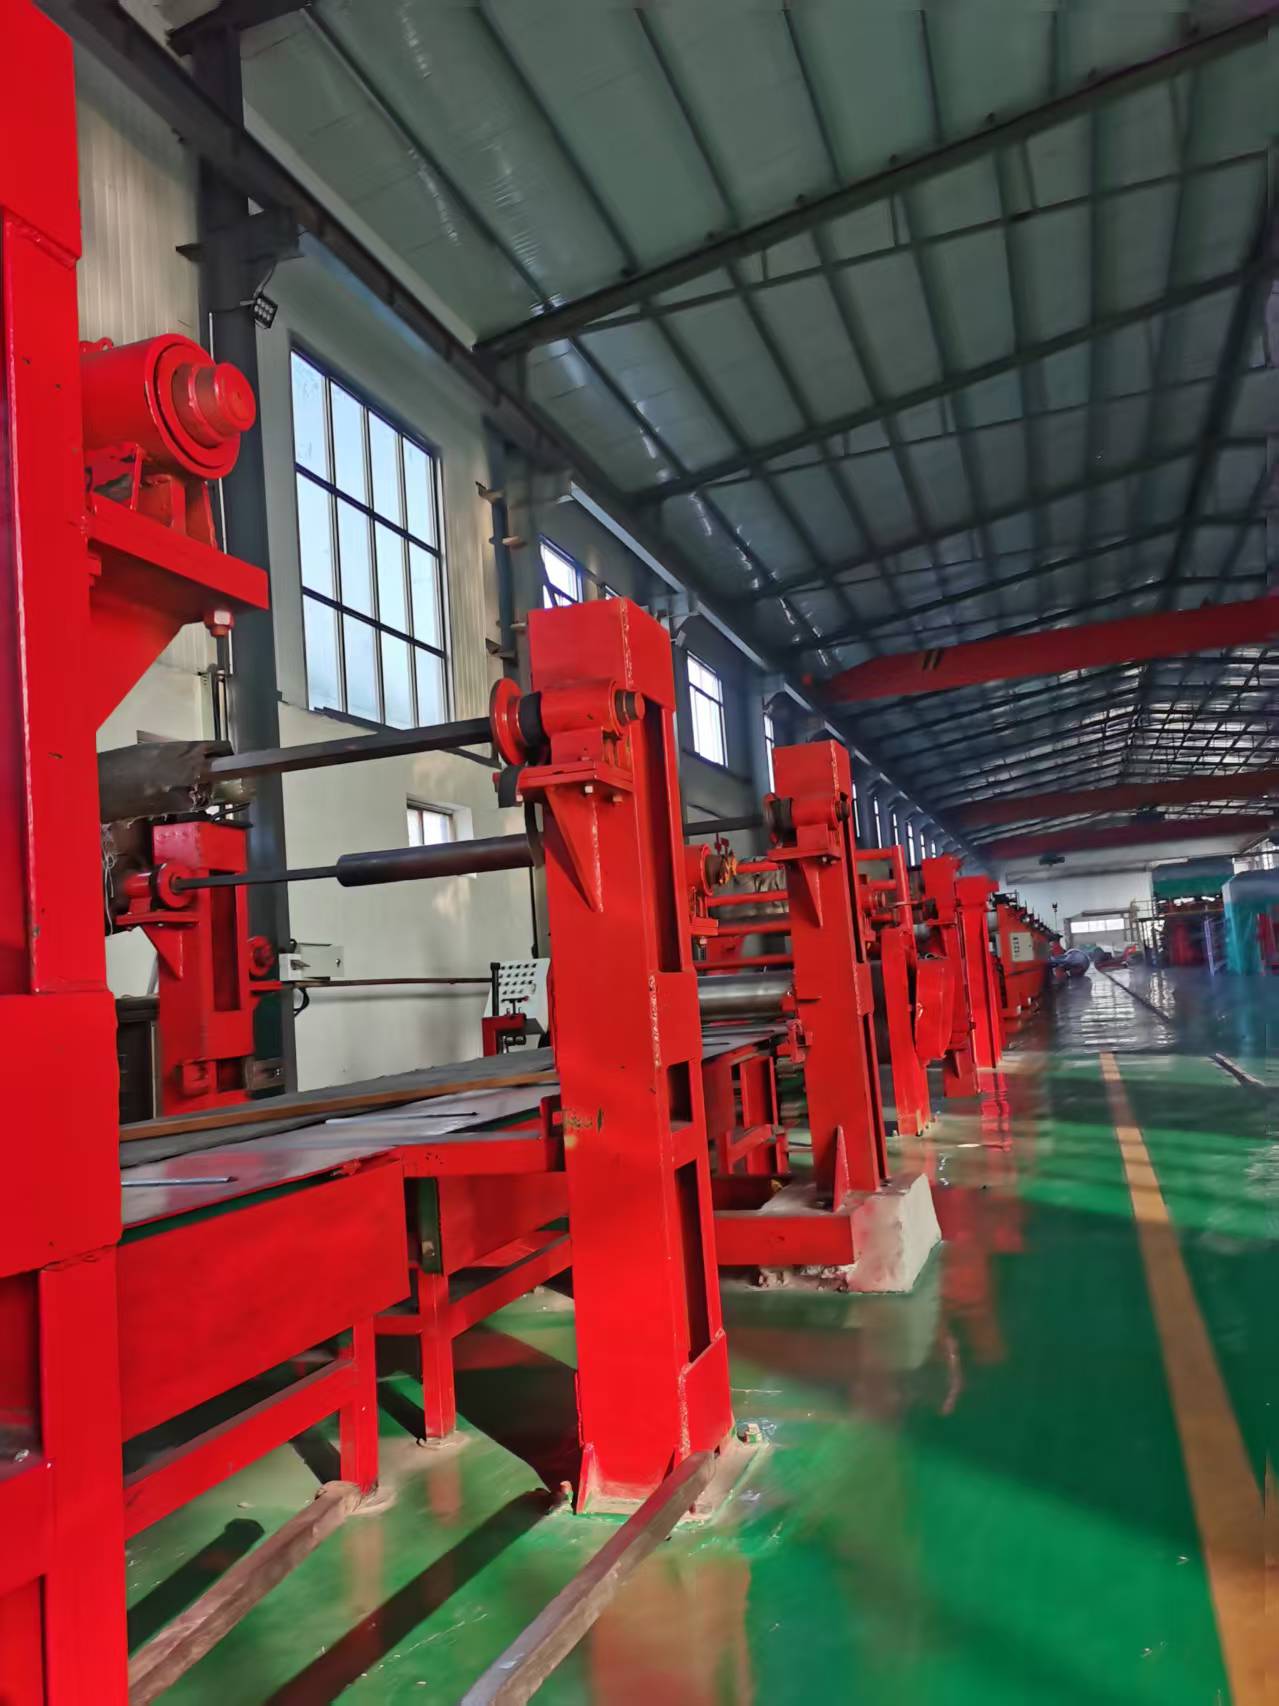
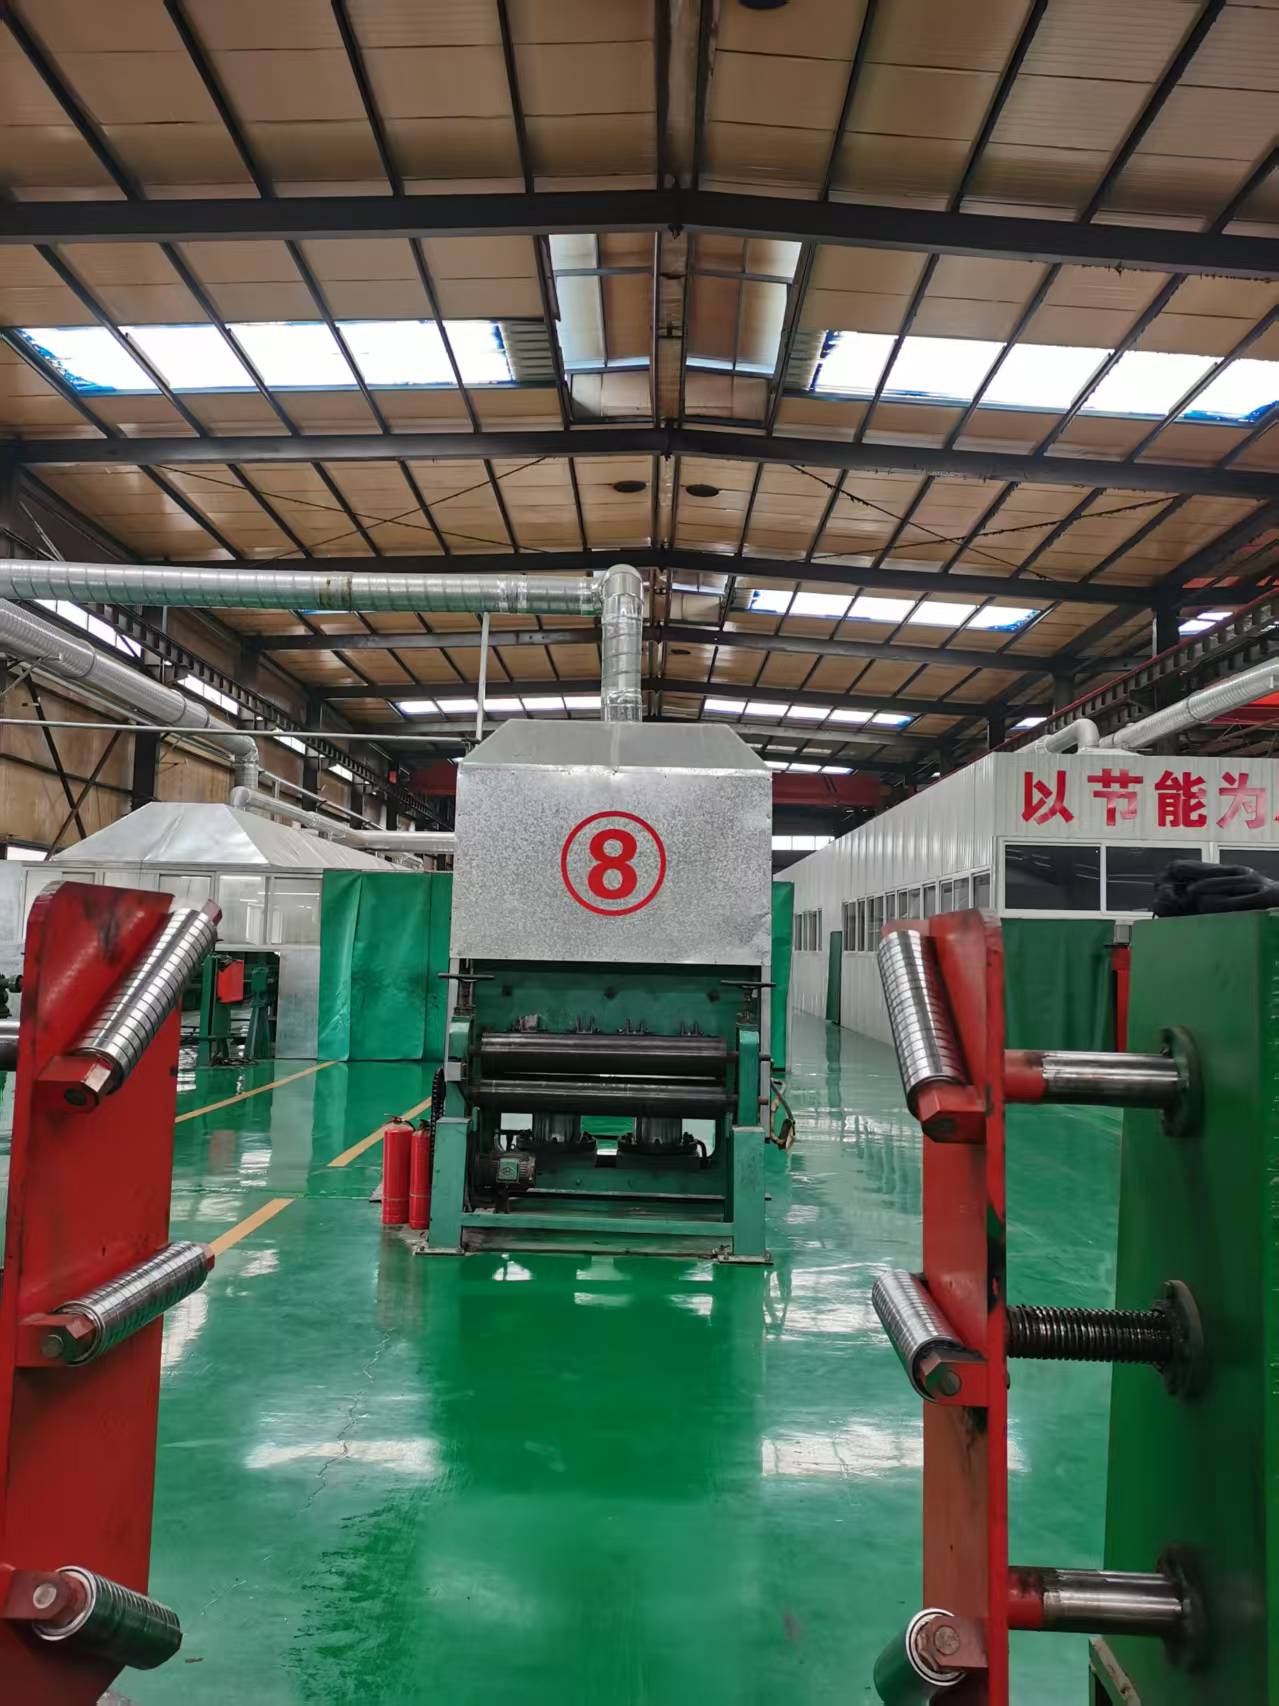
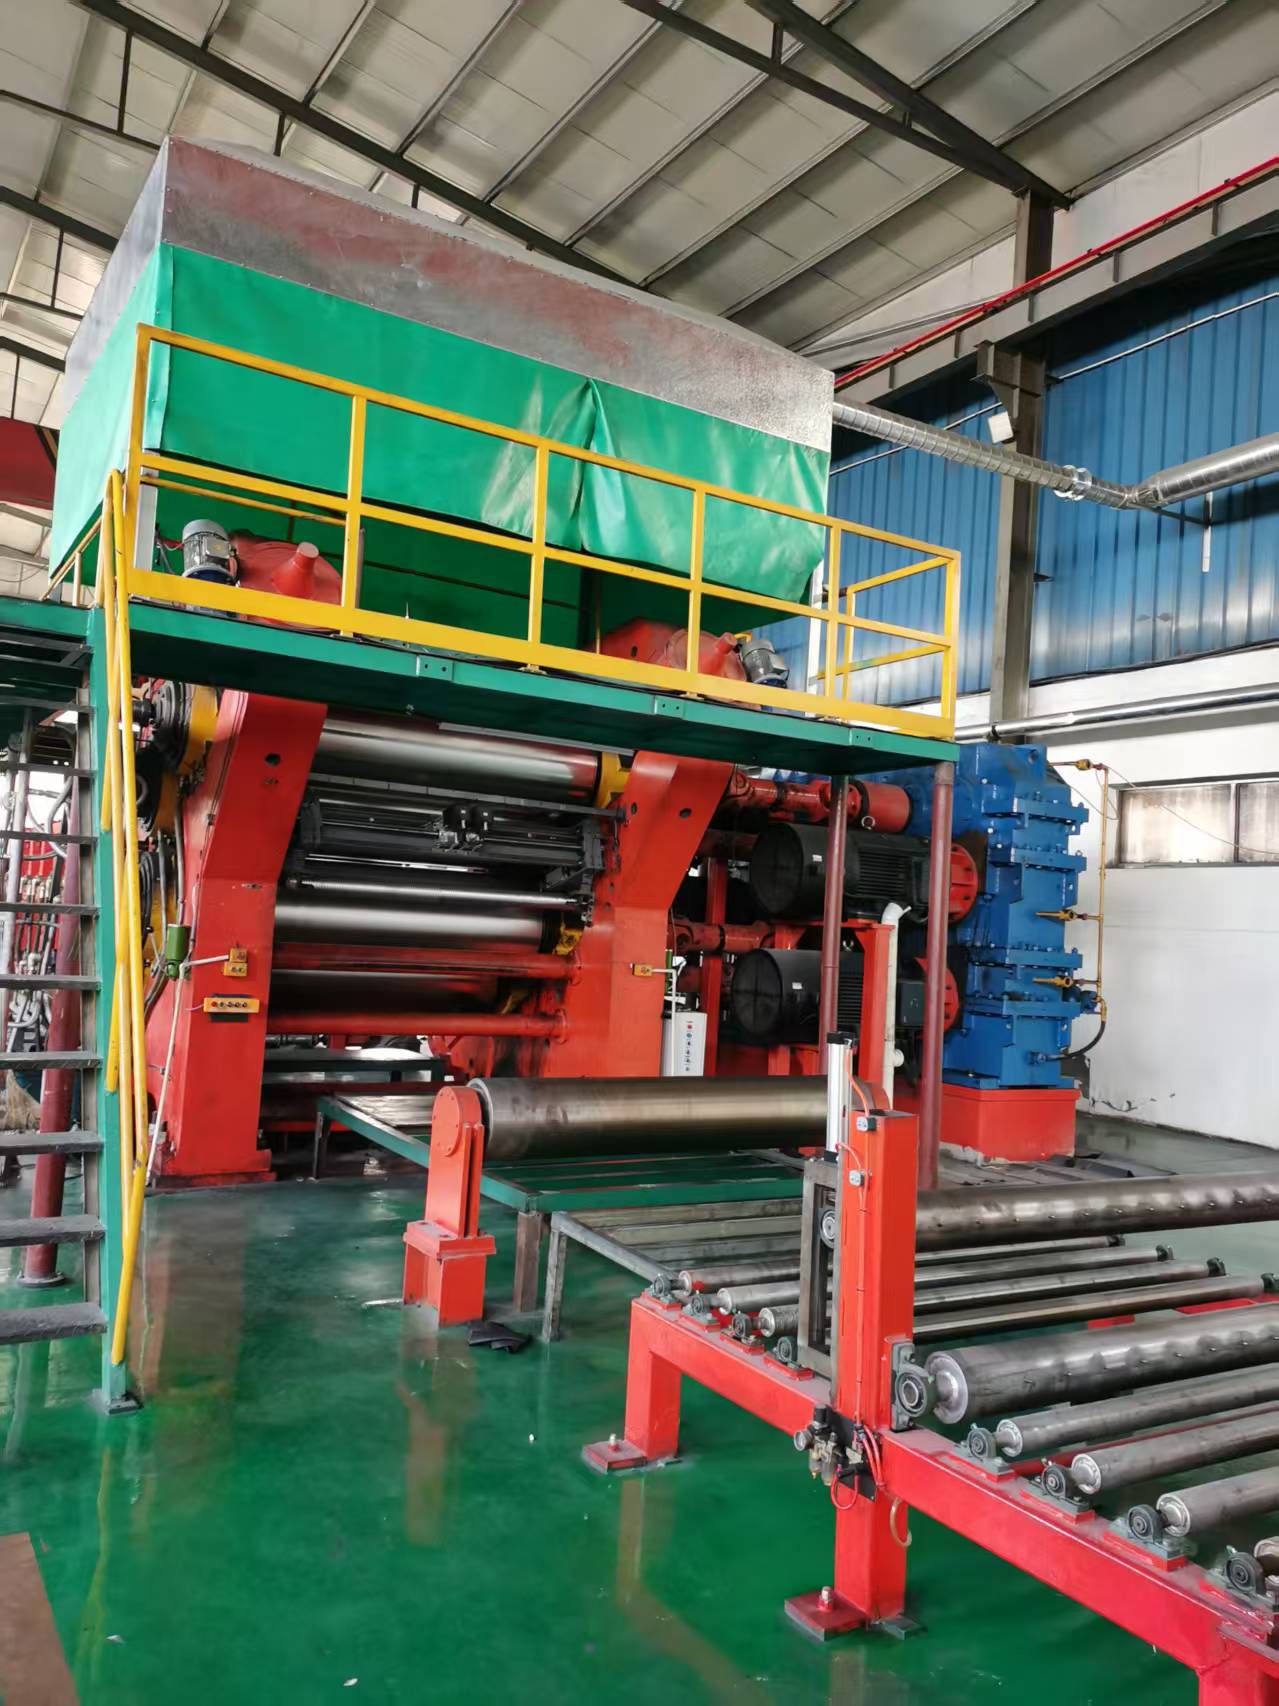
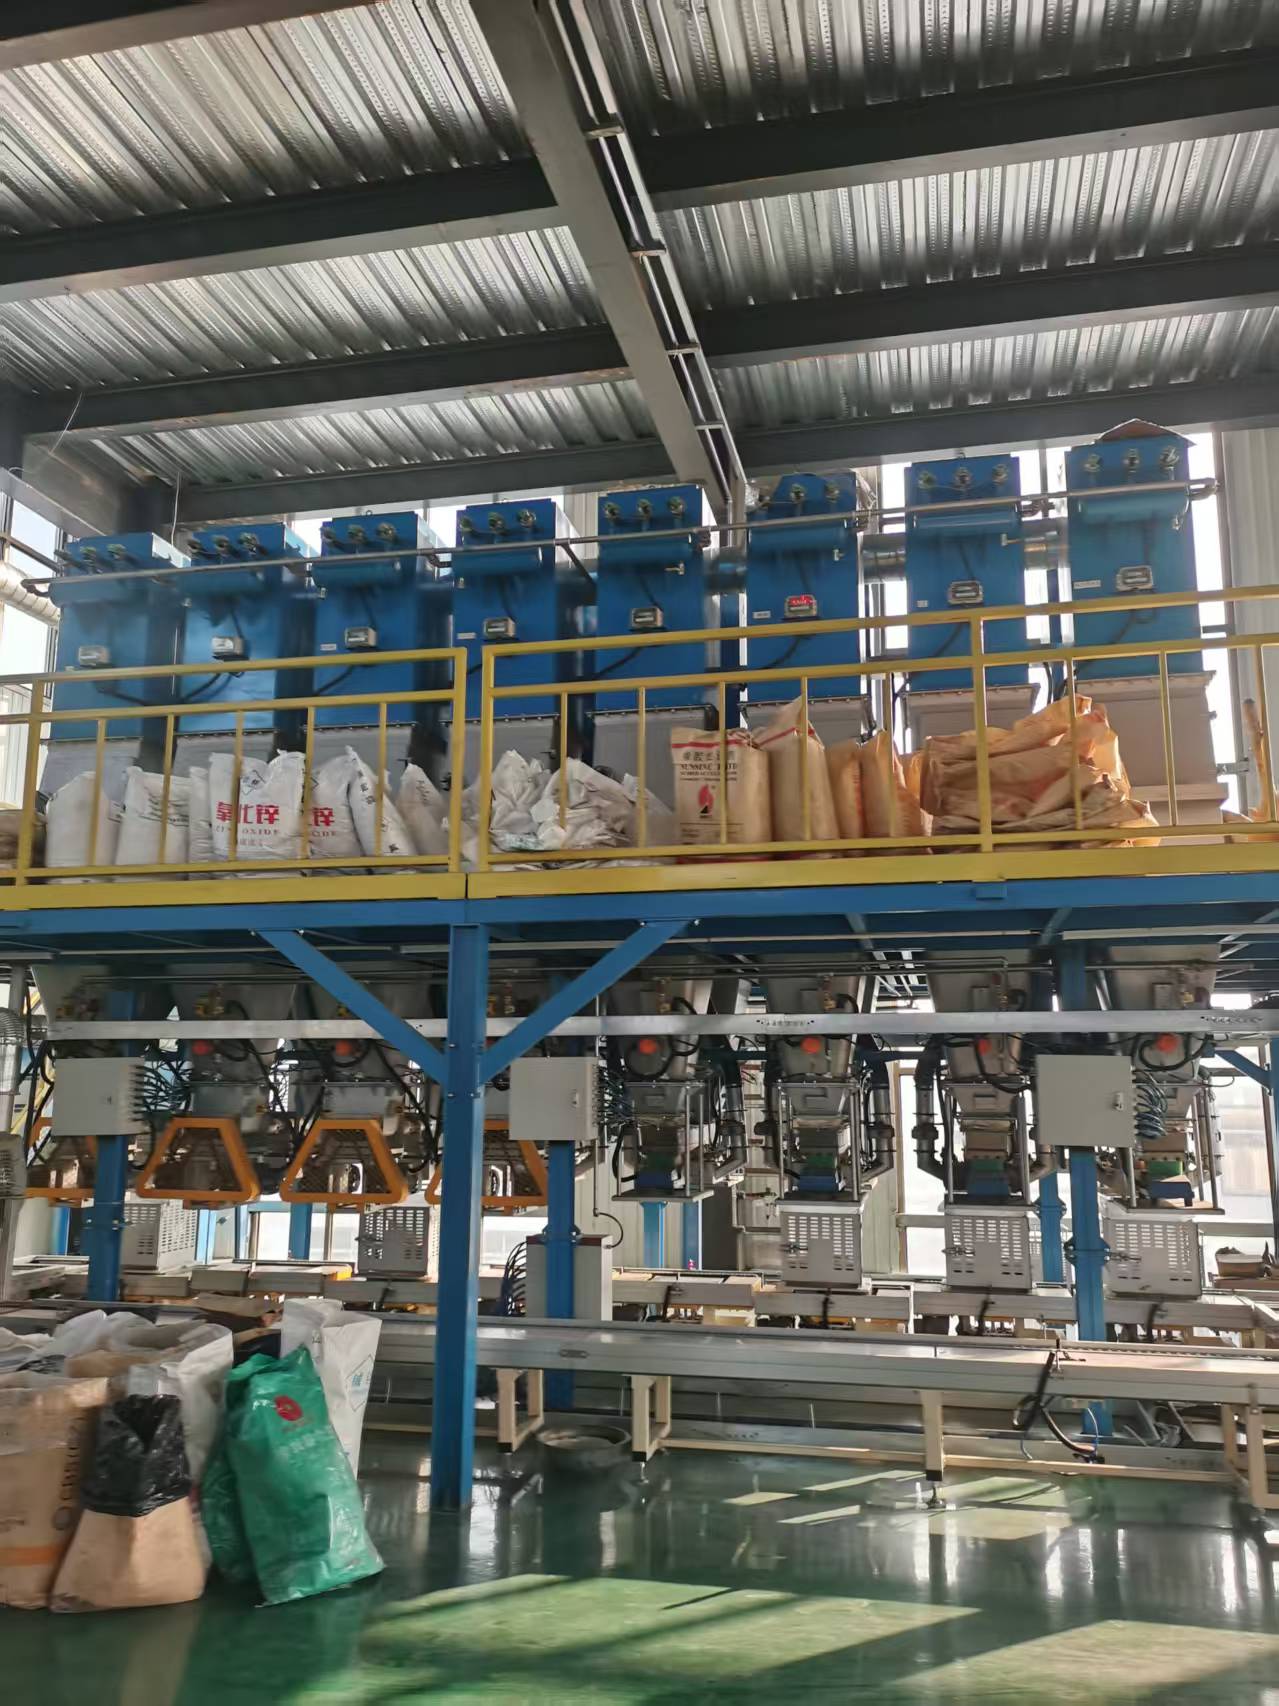
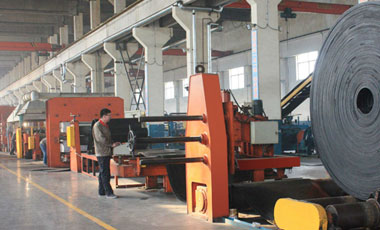
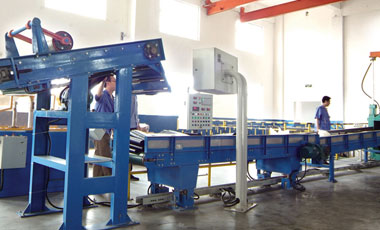
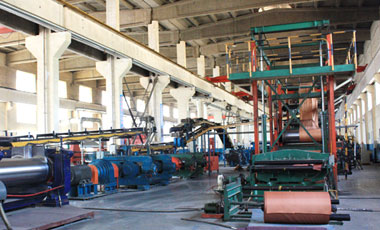
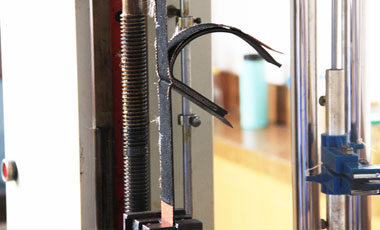
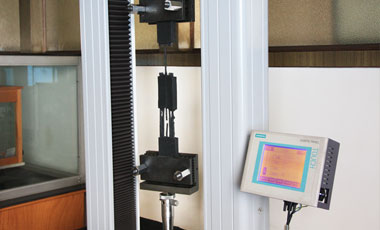
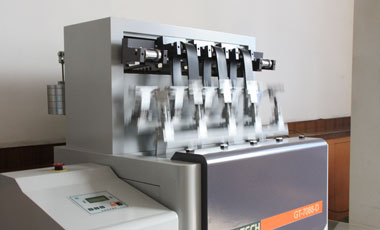
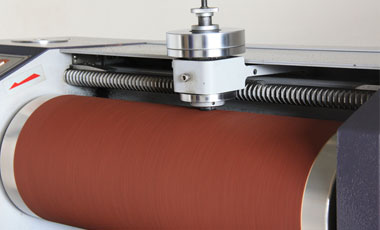
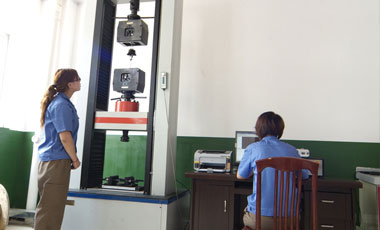
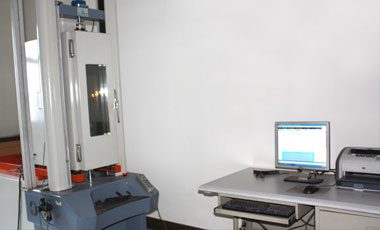
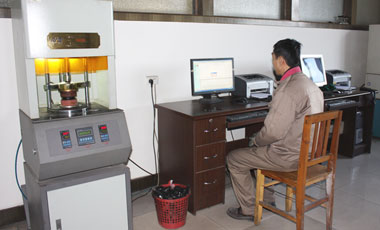
To maintain our reputation as a top-tier rubber belts manufacturer for the London market, we invest heavily in cutting-edge machinery and rigorous testing protocols.
The industrial landscape of the UK is transitioning rapidly towards automation and environmental sustainability. In London, this shift is driven by strict decarbonization goals and the Net Zero strategy. Consequently, the rubber belting industry is undergoing a technological revolution. Today's London buyers are not just looking for standard replacement parts; they require intelligent, energy-efficient, and recyclable rubber conveyor systems.
Modern logistics centers in the M25 corridor are increasingly integrating IoT sensors into their conveyor systems. These smart sensors monitor belt wear, tension, and temperature in real-time. As a forward-thinking manufacturer, we design rubber belts that are compatible with magnetic and optical monitoring systems. This allows London operators to transition from reactive maintenance to predictive maintenance, reducing costly unexpected downtime.
Power consumption is a major operational cost for large-scale distribution centers and aggregate processing plants in Greater London. By utilizing specialized low-rolling-resistance rubber compounds on the pulley side of the belt, we help companies reduce their energy consumption by up to 15%. This technology minimizes indentation rolling resistance as the belt passes over the idlers, translating to direct cost savings and lower carbon emissions.
London's high labor costs make frequent belt replacements economically unviable. Our dynamic fatigue testing ensures that our belts withstand millions of flex cycles without delamination. The steel cord pull-out machine and peeling test equipment at our factory verify that the internal reinforcement and rubber cover bond seamlessly, ensuring that our belts outlast standard market alternatives even under continuous load.
Safety is paramount, especially in confined spaces like London's underground infrastructure and tunneling projects. Our flame-retardant rubber conveyor belts are tested to meet rigorous safety classifications, ensuring they self-extinguish and emit low smoke in the event of a fire. Similarly, our cold-resistant belts maintain their flexibility and strength in freezing winter conditions, preventing cracking and structural failure.
Browse our comprehensive selection of rubber belts designed for the London industrial, construction, and commercial markets.
Designed for handling hot bulk materials up to 200°C in industrial processing plants.
View Details
High-safety belting for underground tunnels, mining, and enclosed logistics hubs.
View Details
Maintains elastomeric properties in sub-zero environments and outdoor yards.
View Details
Vertical bucket elevator belts designed for space-restricted urban building sites.
View Details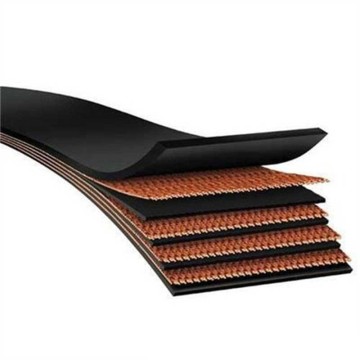
High-elasticity fabric core conveyor belt offering superior resistance to impact wear.
View Details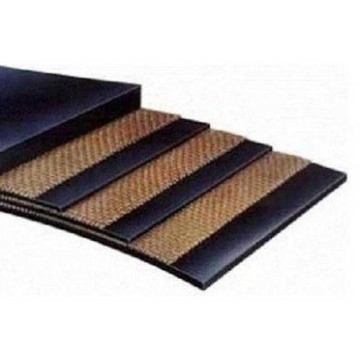
Versatile, cost-effective rubber belting for standard material handling lines.
View Details
Heavy-duty heat-resistant belting optimized for London’s asphalt recycling plants.
View Details
Engineered to meet the highest safety standards for UK underground logistics networks.
View DetailsSelecting the right rubber belt manufacturer is a critical decision that directly impacts your operational efficiency and bottom line. With years of experience serving the London industrial market, we have developed a deep understanding of the unique challenges faced by local businesses. From strict environmental compliance to the need for rapid delivery and minimized downtime, we are committed to providing solutions that exceed expectations.
Our state-of-the-art manufacturing facility is equipped with the latest production and testing machinery, allowing us to maintain strict quality control at every stage of the manufacturing process. Whether you require standard general-purpose belts for a warehousing facility in West London, or highly specialized flame-retardant belts for an underground infrastructure project in Central London, we have the technical expertise and production capacity to deliver high-quality solutions on time and within budget.
We offer comprehensive technical support, from initial belt selection and system design to installation guidance and troubleshooting. Our team of experienced engineers works closely with London clients to ensure that every conveyor belt is optimized for their specific application, reducing wear and tear, lowering energy consumption, and maximizing service life. Partner with a reliable rubber belts factory and experience the difference that quality and dedication can make to your operations.