+86 18920794106
Leave Your Message
-
Contact WhatsApp
-
 Contact Phone
-
 Contact Email
Premium Quality Solutions for US Industrial Applications
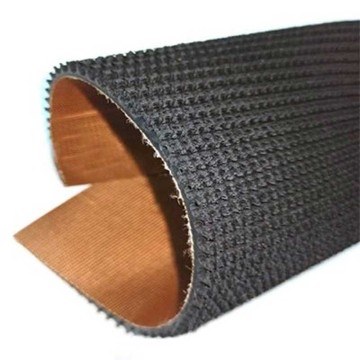
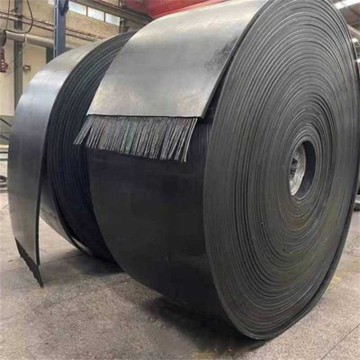
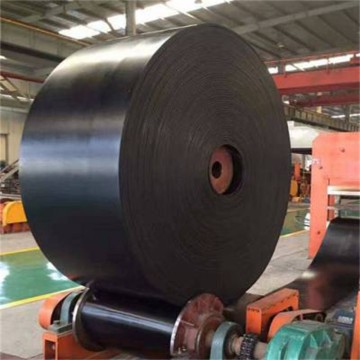
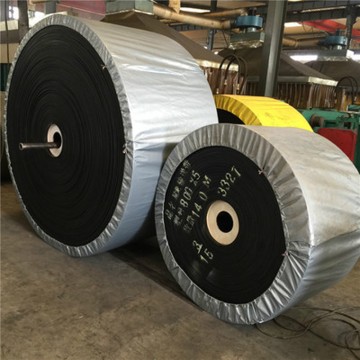
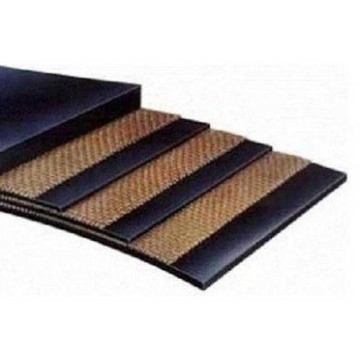
The United States conveyor belt manufacturing industry represents a critical component of the nation's industrial infrastructure, with laminated conveyor belts playing a pivotal role across multiple sectors. The US market for conveyor belts is valued at over $1.8 billion annually, with laminated conveyor belts accounting for a significant portion of this market share. These specialized belts are essential for material handling operations in mining, manufacturing, food processing, logistics, and distribution centers throughout the country.
American industries have increasingly recognized the superior performance characteristics of laminated conveyor belts, which offer enhanced durability, flexibility, and resistance to various operational challenges. The manufacturing landscape in the United States has evolved to meet stringent quality standards, environmental regulations, and the demanding requirements of modern industrial applications. Major manufacturing hubs are located in the Midwest, Southeast, and Western regions, strategically positioned to serve key industrial clusters.
The conveyor belt manufacturing sector in the US employs advanced technologies and adheres to rigorous quality control standards set by organizations such as the Rubber Manufacturers Association (RMA) and the Conveyor Equipment Manufacturers Association (CEMA). These standards ensure that laminated conveyor belts produced in American facilities meet or exceed international benchmarks for safety, performance, and reliability.
The United States mining industry, particularly in states like Wyoming, West Virginia, Kentucky, and Arizona, relies heavily on laminated conveyor belts for transporting coal, minerals, and aggregates. These belts must withstand extreme conditions including abrasive materials, heavy loads, and variable weather conditions. American mining operations demand conveyor belts with superior tear resistance, impact absorption, and long service life to minimize downtime and maximize operational efficiency.
The US food processing sector, concentrated in California, Texas, Iowa, and the Midwest agricultural belt, requires FDA-compliant laminated conveyor belts that meet strict hygiene standards. These belts are used in meat processing plants, dairy facilities, grain handling operations, and produce packaging centers. The belts must be easy to clean, resistant to oils and fats, and capable of operating in temperature-controlled environments while maintaining food safety standards.
American automotive manufacturing plants in Michigan, Ohio, Tennessee, and South Carolina utilize laminated conveyor belts for assembly line operations. The aerospace industry in Washington, California, and Texas also depends on precision conveyor systems for component handling. These applications require belts with consistent tracking, minimal elongation, and the ability to handle diverse product weights and sizes.
The explosive growth of e-commerce has transformed the logistics landscape in the United States, with major distribution hubs operated by companies like Amazon, Walmart, and FedEx requiring sophisticated conveyor systems. States like Pennsylvania, New Jersey, California, and Texas host massive fulfillment centers where laminated conveyor belts facilitate high-speed sorting, routing, and package handling operations. These facilities demand belts with excellent flexibility, low noise operation, and compatibility with automated systems.
Major US airports including Atlanta Hartsfield-Jackson, Los Angeles International, Chicago O'Hare, and Dallas/Fort Worth utilize extensive conveyor belt systems for baggage handling. These applications require laminated belts with high reliability, smooth operation, and the ability to handle varying load configurations while meeting TSA security requirements.
Heavy-duty solutions for coal, minerals, and aggregate transportation across US mining operations
FDA-compliant belts for meat, dairy, grain, and produce handling facilities
Precision conveyor systems for automotive, aerospace, and industrial assembly
High-speed sorting and distribution solutions for modern fulfillment centers
Reliable baggage handling for major US transportation hubs
Durable belts for concrete, asphalt, and building material handling
The American manufacturing sector is experiencing a significant shift toward Industry 4.0 principles, with conveyor belt systems incorporating IoT sensors, predictive maintenance capabilities, and real-time monitoring. Laminated conveyor belts are being designed with embedded sensors that can detect wear patterns, track belt tension, and predict maintenance needs before failures occur. This trend is particularly prominent in high-tech manufacturing facilities and modern distribution centers across the United States.
Environmental consciousness is driving innovation in conveyor belt manufacturing, with US companies increasingly focusing on sustainable materials, reduced energy consumption, and recyclability. California's strict environmental regulations and the growing emphasis on corporate sustainability across the nation are pushing manufacturers to develop eco-friendly laminated conveyor belts using recycled rubber compounds and low-emission manufacturing processes. Energy-efficient belt designs that reduce friction and power consumption are becoming industry standards.
The diverse nature of American industries demands highly customized conveyor belt solutions. Manufacturers are investing in advanced engineering capabilities to develop application-specific laminated belts that address unique operational challenges. This includes belts with specialized surface textures for inclined transport, antimicrobial properties for food processing, antistatic properties for electronics manufacturing, and fire-resistant compounds for underground mining operations.
Research and development efforts in the United States are focusing on next-generation materials that enhance the performance characteristics of laminated conveyor belts. This includes the integration of aramid fibers for increased strength-to-weight ratios, thermoplastic elastomers for improved flexibility, and nano-composite materials for enhanced wear resistance. American manufacturers are collaborating with universities and research institutions to develop breakthrough materials that extend belt life and reduce total cost of ownership.
Recent trends toward reshoring and domestic manufacturing are creating new opportunities for US-based conveyor belt manufacturers. Government initiatives promoting American manufacturing, coupled with supply chain disruptions experienced during global crises, have reinforced the value of local production capabilities. This trend is expected to drive investment in domestic manufacturing facilities and create jobs across the conveyor belt industry supply chain.
Modern warehouses and manufacturing facilities are increasingly integrating conveyor systems with robotic picking systems and AGVs. Laminated conveyor belts are being designed to work seamlessly with these automated systems, featuring precise tracking capabilities, consistent surface properties, and compatibility with vision systems and barcode scanners. This integration is particularly evident in cutting-edge facilities operated by technology companies and major retailers.
The United States features distinct regional clusters for conveyor belt manufacturing and consumption. The Midwest, particularly Ohio, Indiana, and Illinois, serves as a major manufacturing hub with strong automotive and heavy machinery industries. The Southeast, including North Carolina, South Carolina, and Georgia, has emerged as a growing manufacturing center with significant textile and automotive operations. The Western states, especially California and Washington, focus on technology, aerospace, and agricultural applications. Texas serves as a critical hub for oil and gas, chemical processing, and logistics operations.
US manufacturers must navigate a complex regulatory landscape including OSHA workplace safety requirements, EPA environmental standards, and industry-specific regulations such as MSHA standards for mining applications and FDA requirements for food-contact applications. Compliance with these regulations drives continuous improvement in belt design, manufacturing processes, and quality control systems. American manufacturers have developed expertise in meeting these stringent requirements, positioning them as leaders in safety and quality standards.
The conveyor belt manufacturing industry in the United States maintains a sophisticated supply chain network encompassing raw material suppliers, component manufacturers, and distribution partners. Key raw materials including synthetic rubber, textile reinforcements, and steel cord are sourced both domestically and internationally. Recent emphasis on supply chain resilience has prompted manufacturers to diversify supplier relationships and maintain strategic inventory levels to ensure uninterrupted production.
The US conveyor belt market features both large multinational corporations and specialized regional manufacturers. Competition drives innovation, quality improvement, and customer service excellence. American manufacturers differentiate themselves through technical expertise, rapid response times, customization capabilities, and comprehensive after-sales support including installation services, maintenance training, and emergency repair capabilities.
State-of-the-Art Production and Testing Facilities
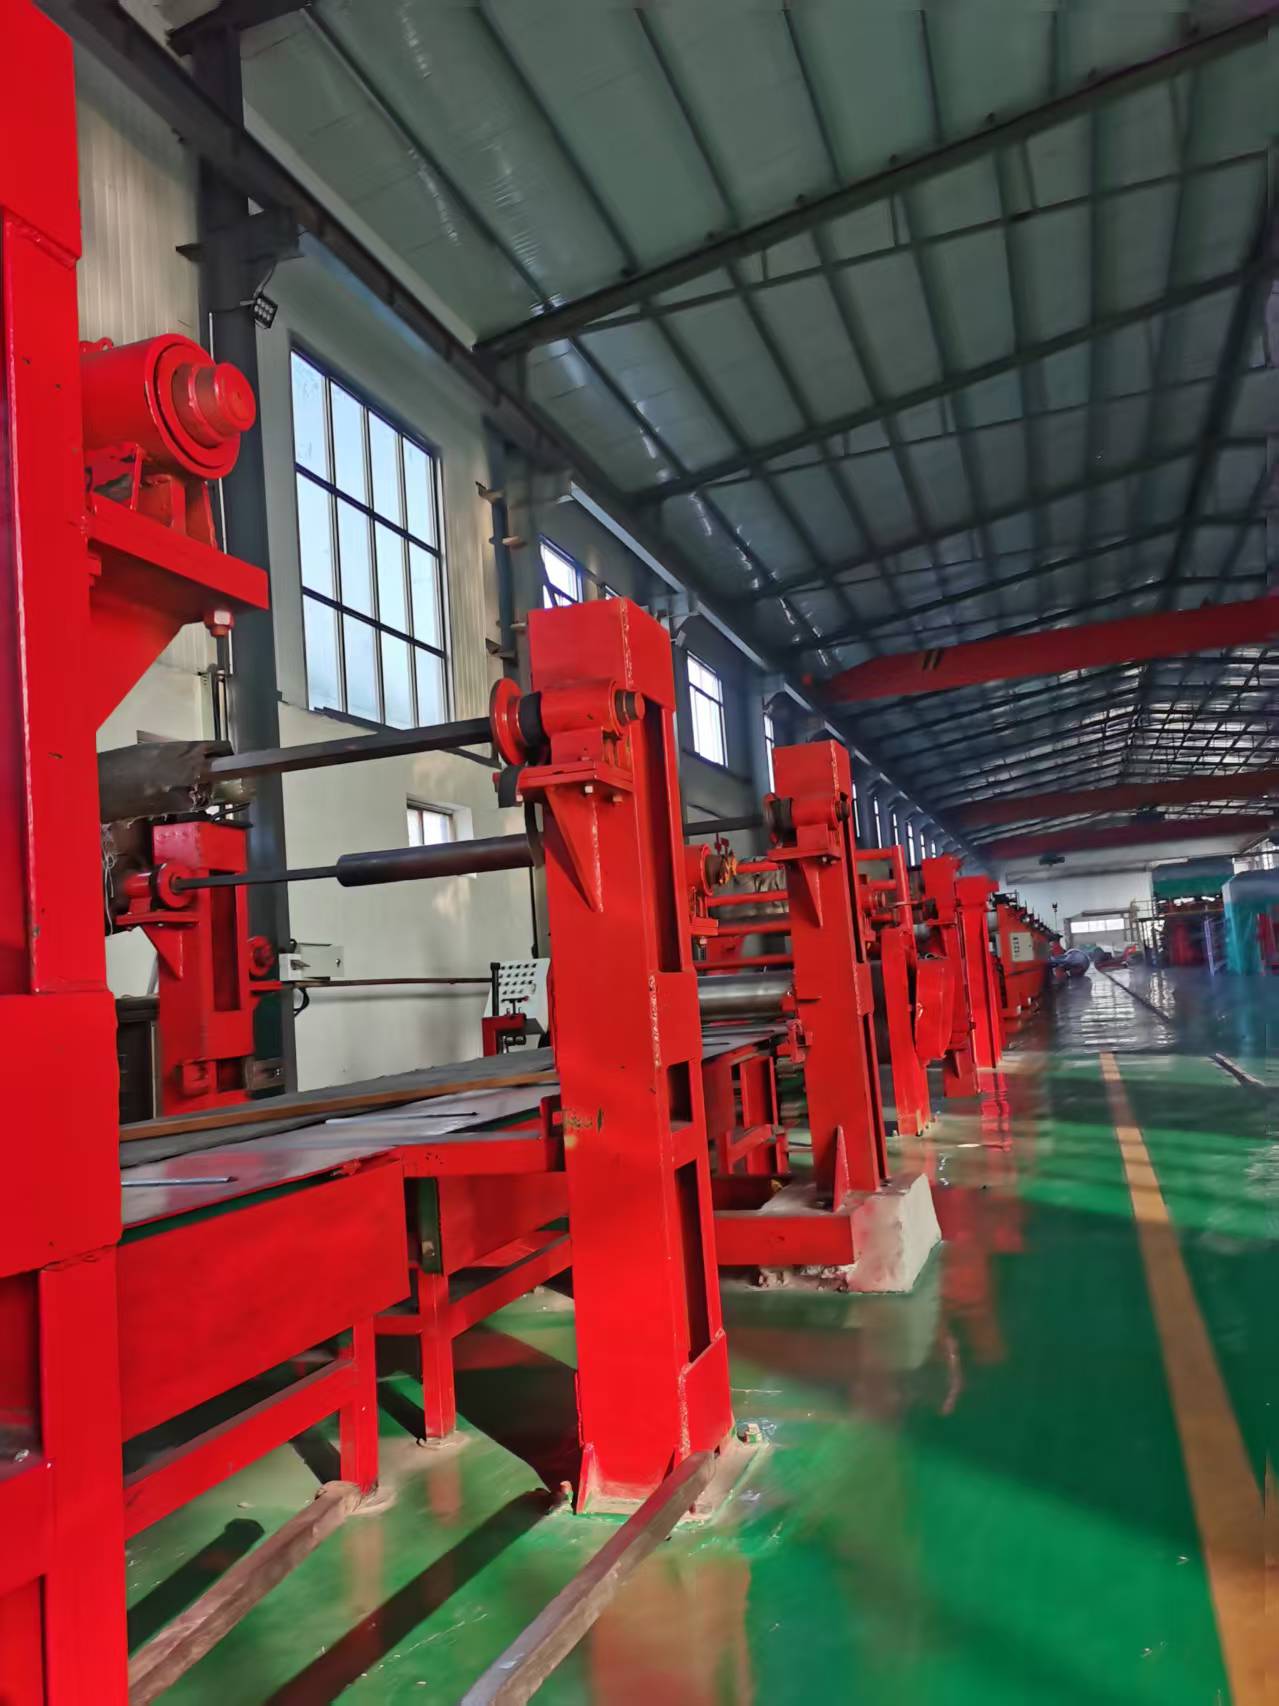
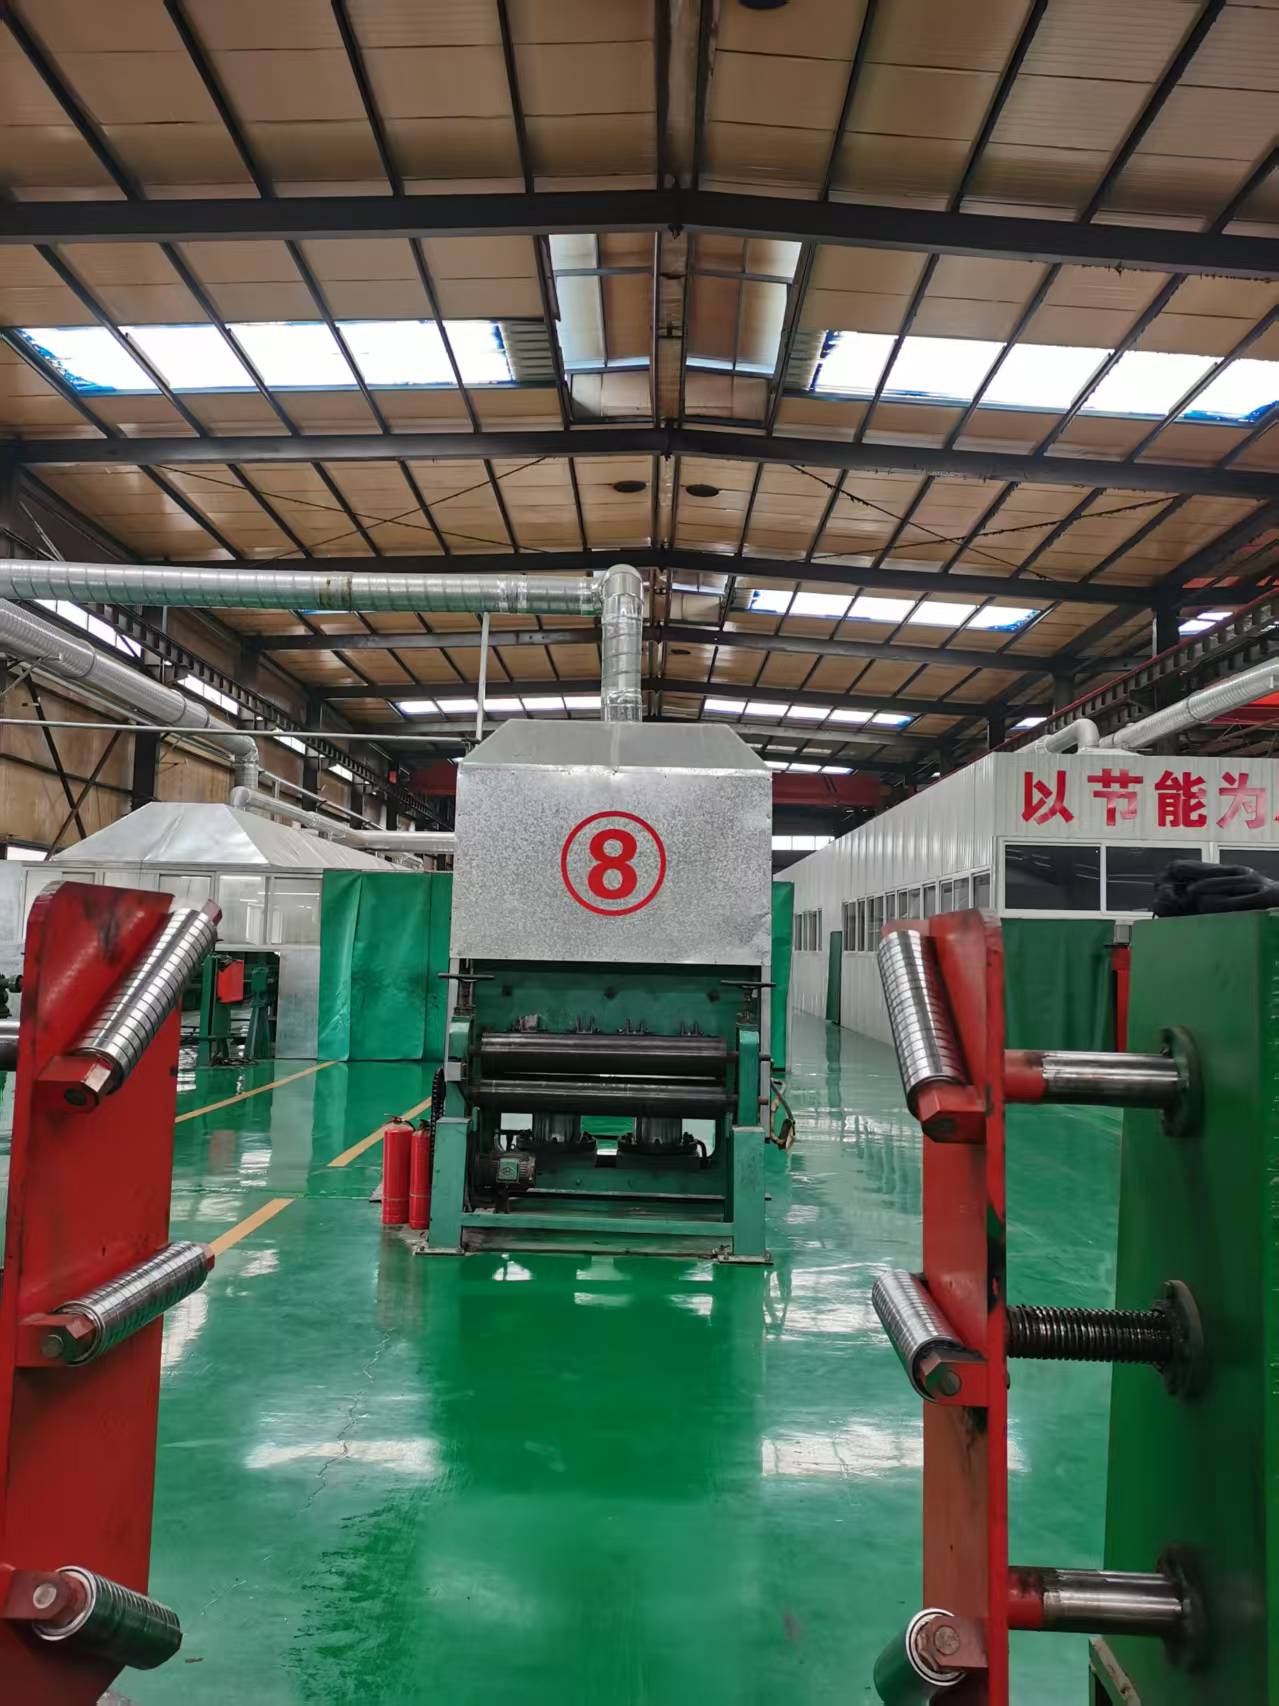
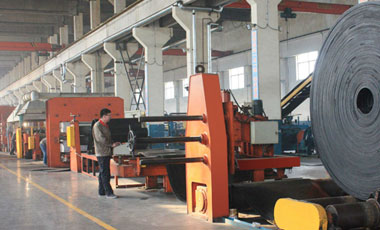
Production Line of Fabric Conveyor Belt
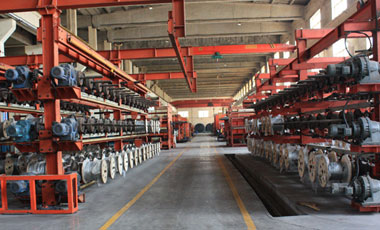
Production Equipment of Steel Cord Conveyor Belt
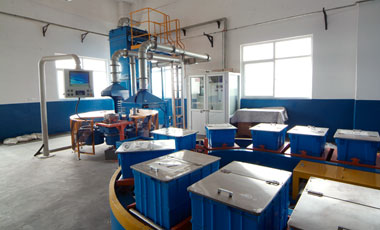
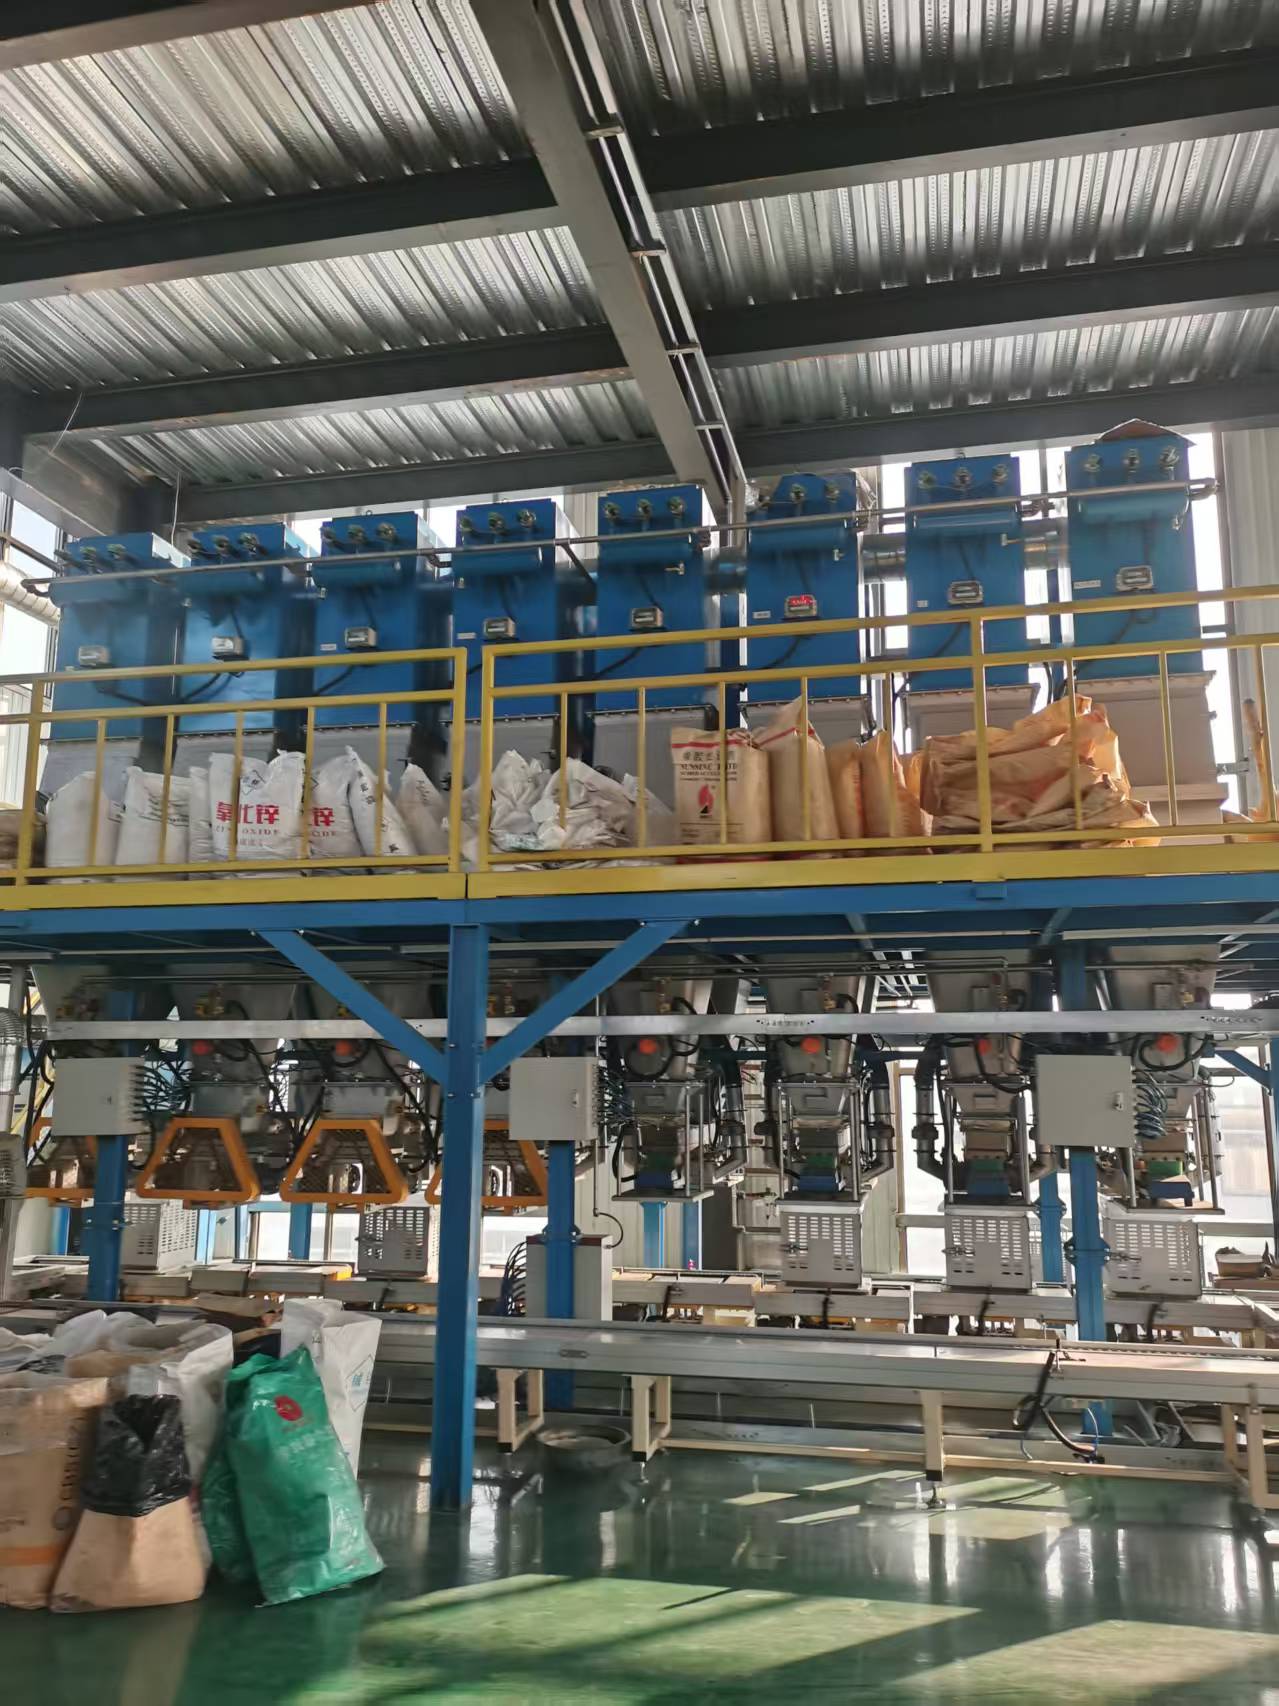
Proportioning Room of Mixing Center
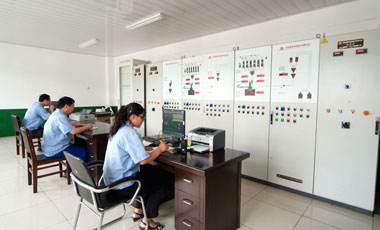
Proportioning System of Mixing Center
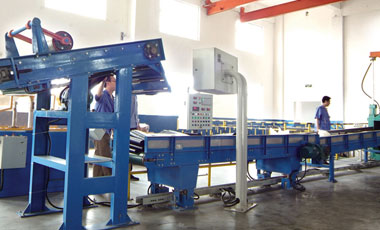
Feeding Device
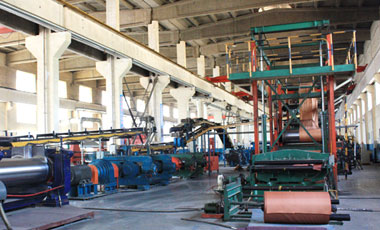
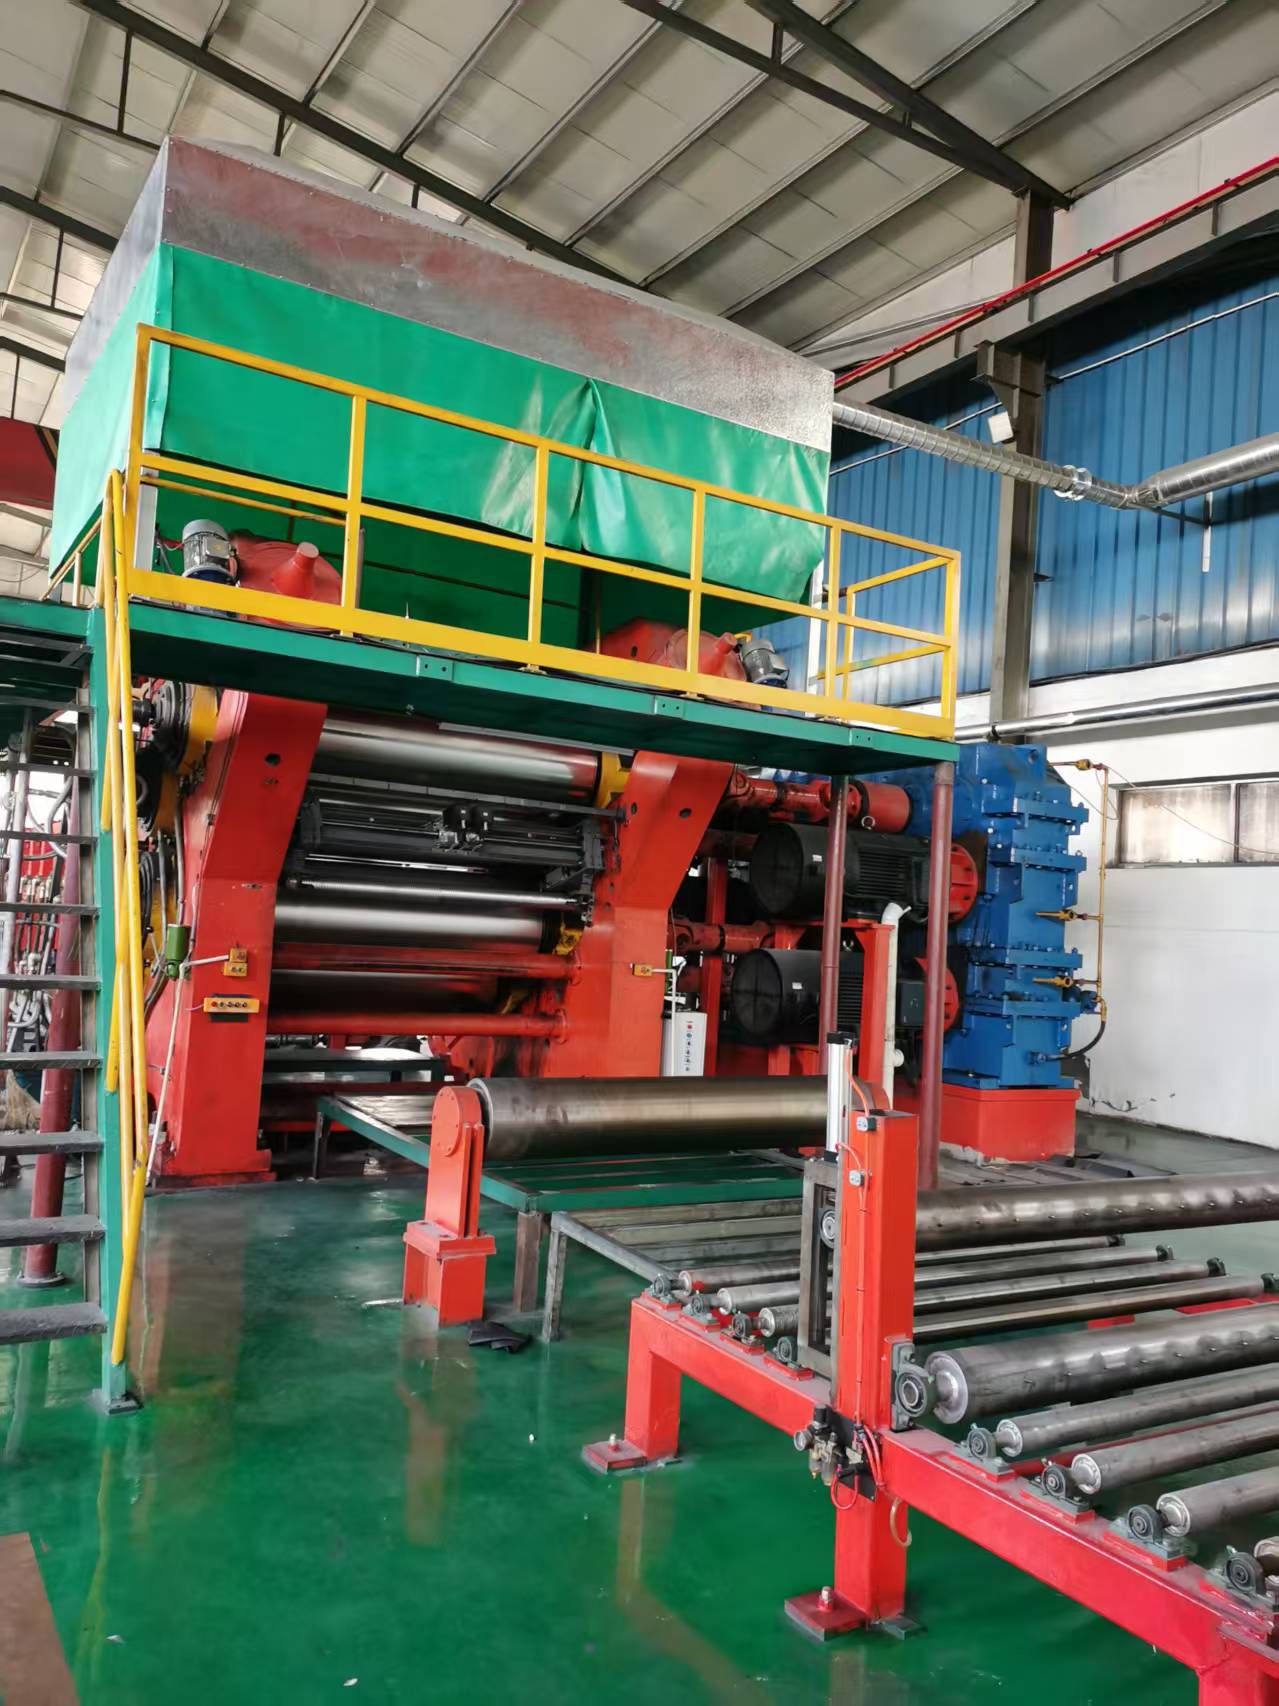
Calendering & Shaping Machine
Our manufacturing facilities utilize cutting-edge production equipment and rigorous quality control processes to ensure every laminated conveyor belt meets the highest standards required by American industries. From automated mixing centers that ensure precise rubber compound formulations to advanced calendering systems that create uniform belt layers, our production capabilities represent the forefront of conveyor belt manufacturing technology.
The production process incorporates multiple quality checkpoints, including real-time monitoring of belt thickness, tension testing, and visual inspection systems. Our fabric conveyor belt production lines feature precision coating systems that ensure optimal adhesion between layers, while our steel cord belt manufacturing equipment maintains exact cord spacing and tension for maximum strength and durability.
Investment in state-of-the-art equipment enables us to serve diverse American industries with customized solutions that meet specific operational requirements, whether for high-temperature applications in steel mills, food-grade requirements in processing facilities, or heavy-duty performance in mining operations.
Comprehensive Conveyor Belt Solutions for Every Application
As the American industrial landscape continues to evolve with increasing automation, sustainability requirements, and operational efficiency demands, the role of high-quality laminated conveyor belts becomes ever more critical. Our commitment to manufacturing excellence, continuous innovation, and customer satisfaction positions us as a trusted partner for US industries seeking reliable conveyor belt solutions.
Whether your operation involves coal mining in Wyoming, food processing in California, automotive assembly in Michigan, or package distribution in Texas, our comprehensive range of laminated conveyor belts delivers the performance, durability, and reliability required for success in today's competitive environment. Our products are engineered to withstand the diverse challenges of American industrial operations while meeting the highest standards for safety, quality, and environmental responsibility.
We invite you to explore our complete product range and discover how our laminated conveyor belt solutions can optimize your material handling operations, reduce downtime, lower maintenance costs, and improve overall operational efficiency. Contact our technical team to discuss your specific requirements and learn how we can customize solutions to meet your unique application needs.
With decades of manufacturing expertise, state-of-the-art production facilities, rigorous quality control, and a deep understanding of American industrial requirements, we stand ready to serve as your preferred conveyor belt supplier. Experience the difference that premium quality laminated conveyor belts can make in your operations.