+86 18920794106
Leave Your Message
-
Contact WhatsApp
-
 Contact Phone
-
 Contact Email
Engineered to withstand extreme environments, our premium conveyor belts serve key sectors across South San Francisco, Oakland, and the wider Bay Area.
Unlocking efficiency across Northern California's premier commercial hubs, cargo ports, and supply chains.
When people think of San Francisco, tech giants and the Golden Gate Bridge often come to mind. However, the Bay Area is also home to a thriving, highly complex industrial ecosystem. From the massive logistics operations at the Port of Oakland to the high-tech manufacturing corridors in South San Francisco, robust material handling systems are the unsung heroes keeping the economy moving.
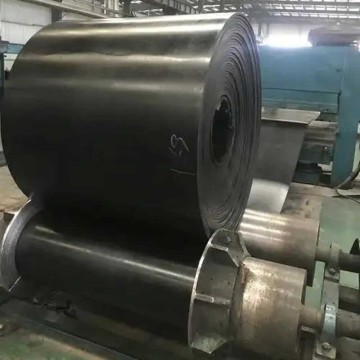
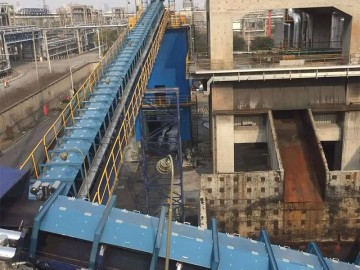
Heavy-duty rubber conveyor belts are essential components in this machinery. Whether it is moving bulk raw materials for aggregate processing, handling baggage at the San Francisco International Airport (SFO), or sorting recyclables at state-of-the-art municipal waste facilities, the demand for high-strength, durable, and reliable rubber belting has never been higher.
As California leads the nation in environmental regulations and green technologies, local industries require rubber belts that are not only durable but also energy-efficient. Modern rubber formulations reduce rolling resistance, which directly lowers the power consumption of massive conveyor systems.
Furthermore, our manufacturing techniques utilize advanced polymer chemistry to ensure that our belts emit zero toxic outgassings, making them suitable for the strict environmental standards of the San Francisco Bay Area Air Quality Management District (BAAQMD).
We are actively bridging the gap between traditional manufacturing and digital transformation. Our heavy-duty rubber belts are designed to seamlessly integrate with modern IoT sensors and AI-driven predictive maintenance systems, allowing Bay Area operators to monitor belt wear, tension, and temperature in real-time, preventing costly unscheduled downtime.
From marine terminals to high-tech recycling centers, discover how our custom-fabricated belts perform in local environments.
The salty, humid air of the San Francisco Bay demands rubber belting with superior ozone and oxidation resistance. Our marine-grade belts handle bulk commodities, chemical fertilizers, and salt aggregates with zero structural degradation.
San Francisco is a global pioneer in zero-waste initiatives. Our puncture-resistant and oil-resistant rubber belts are engineered to withstand sharp glass, metals, and organic oils found in municipal sorting and recovery facilities.
With ongoing transit improvements and underground developments across the Bay, our high-tensile steel cord and flame-retardant rubber belts provide critical safety and heavy lifting capacities for deep excavation projects.
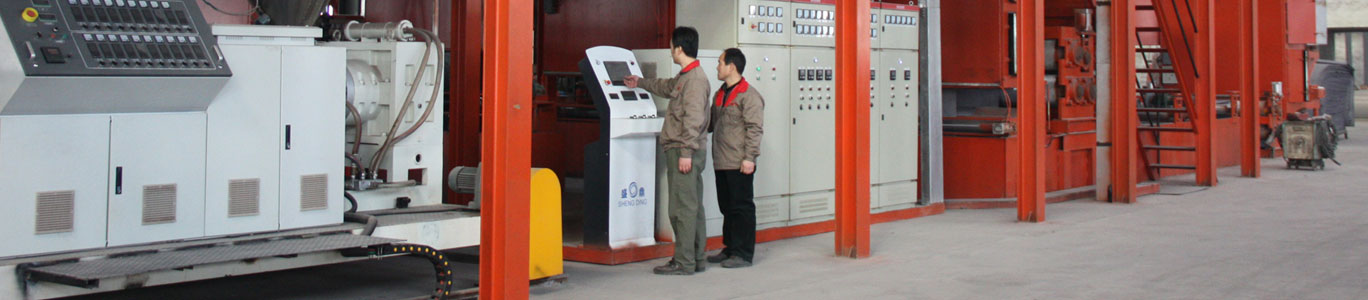
Explore our world-class manufacturing plant equipped with cutting-edge machinery to guarantee the highest quality standards for every batch shipped to San Francisco.
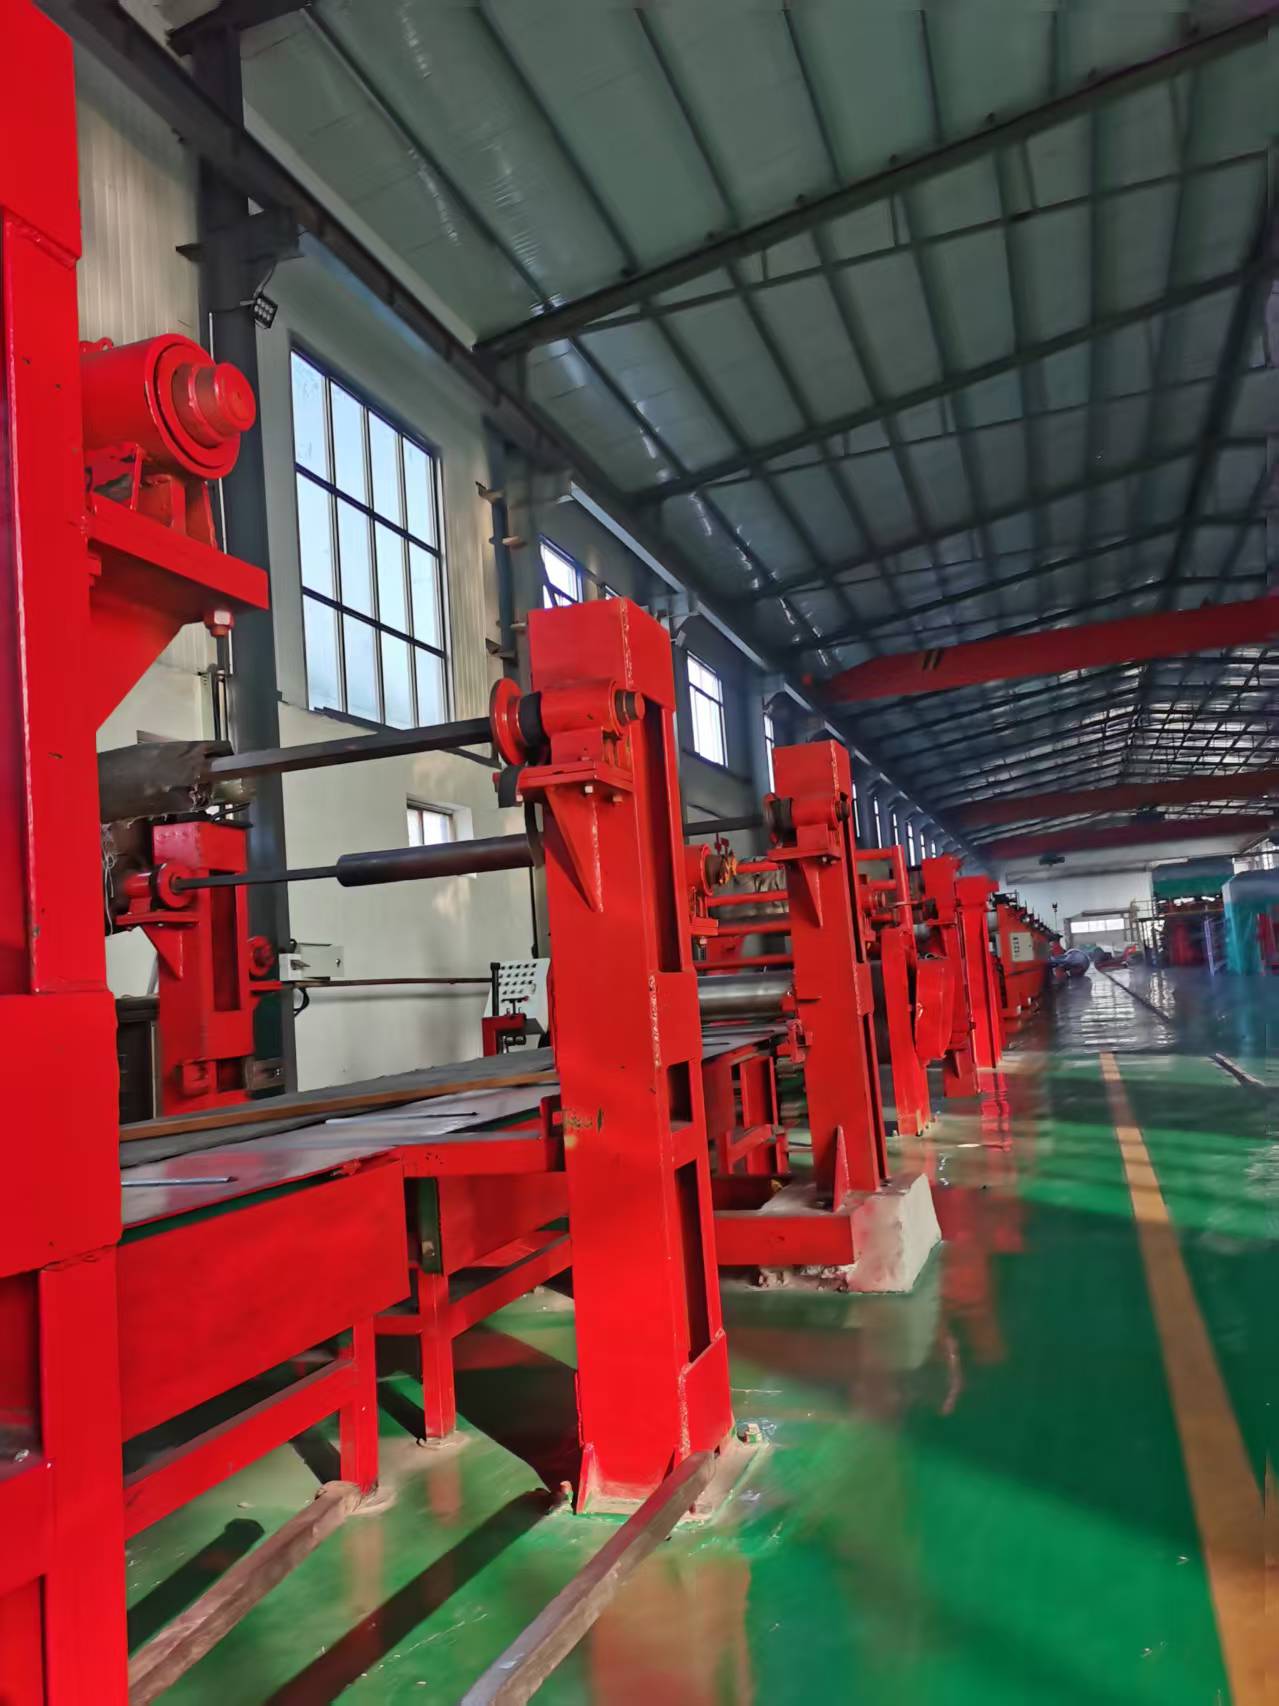
Heavy Duty Vulcanizing Press
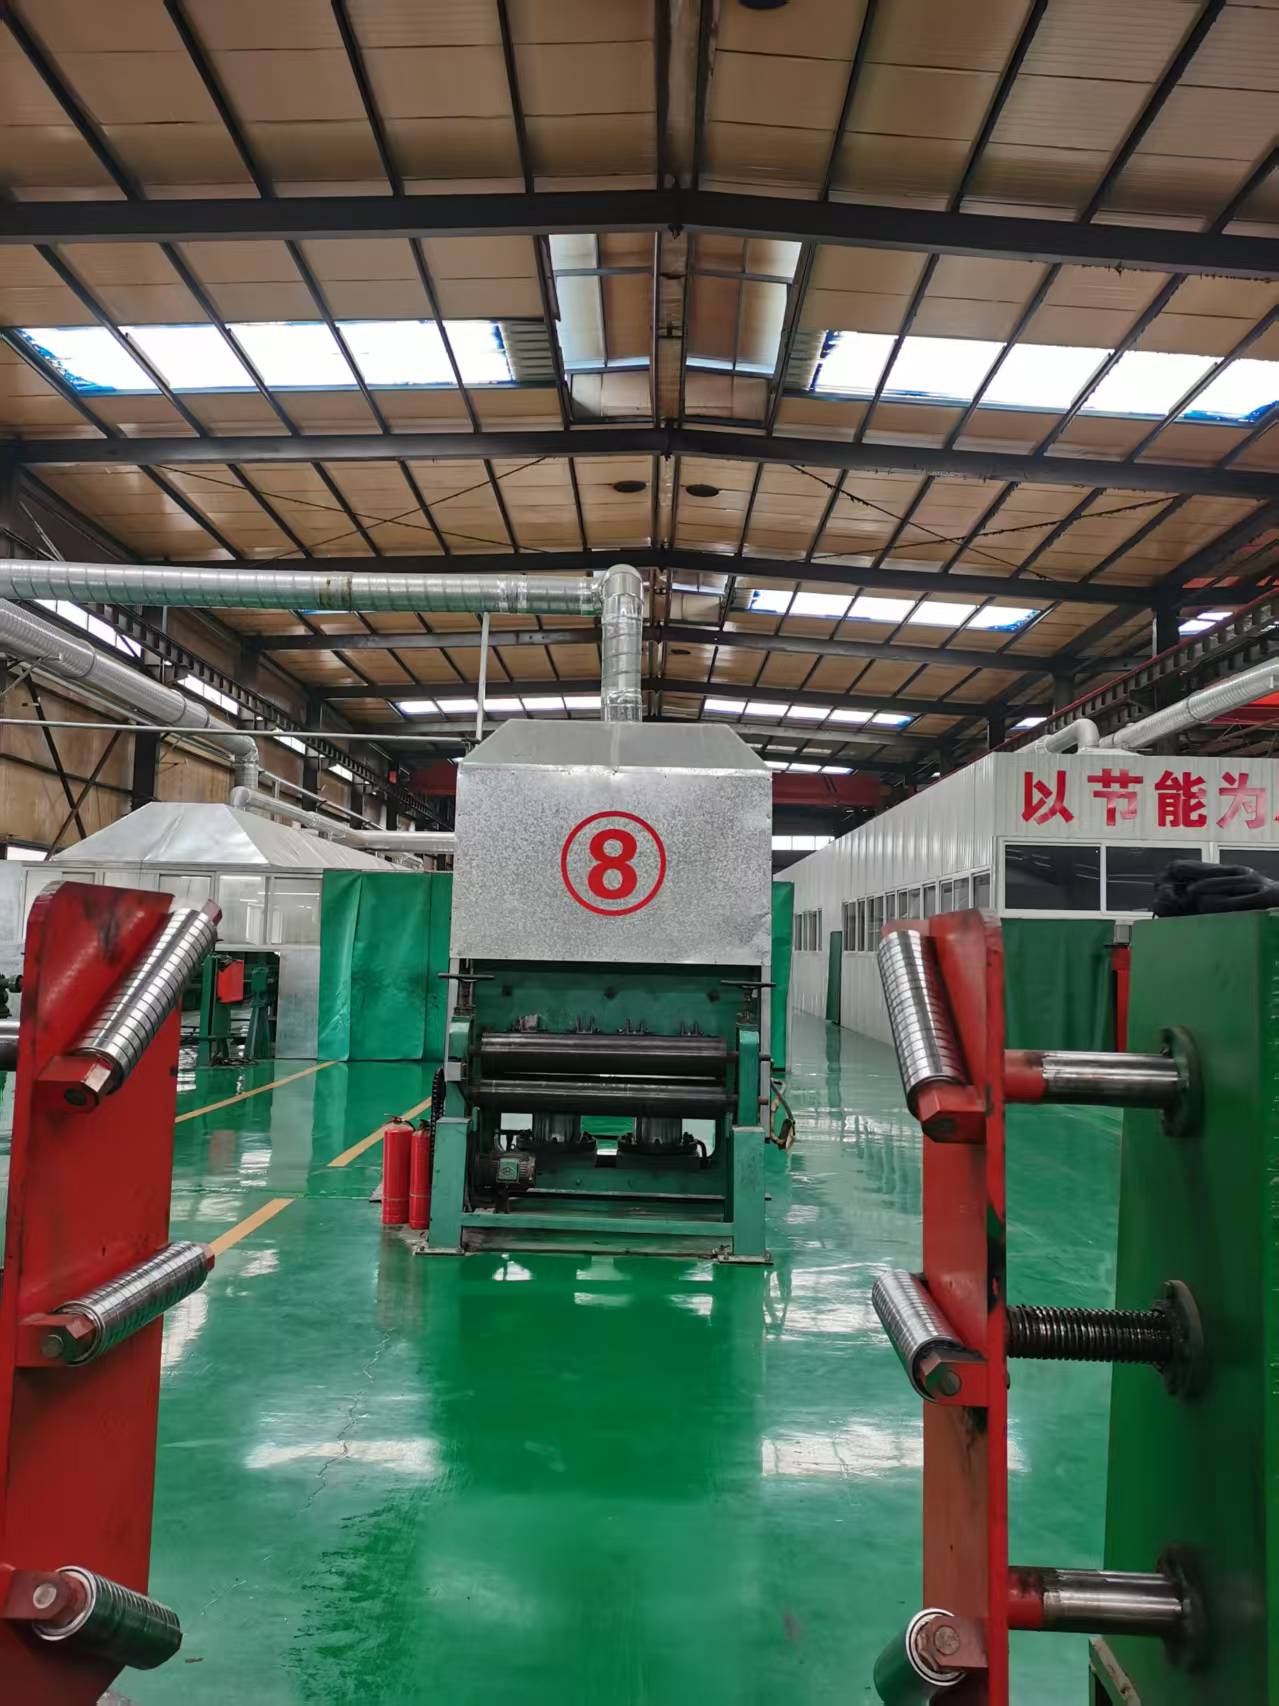
Precision Rubber Calendaring System
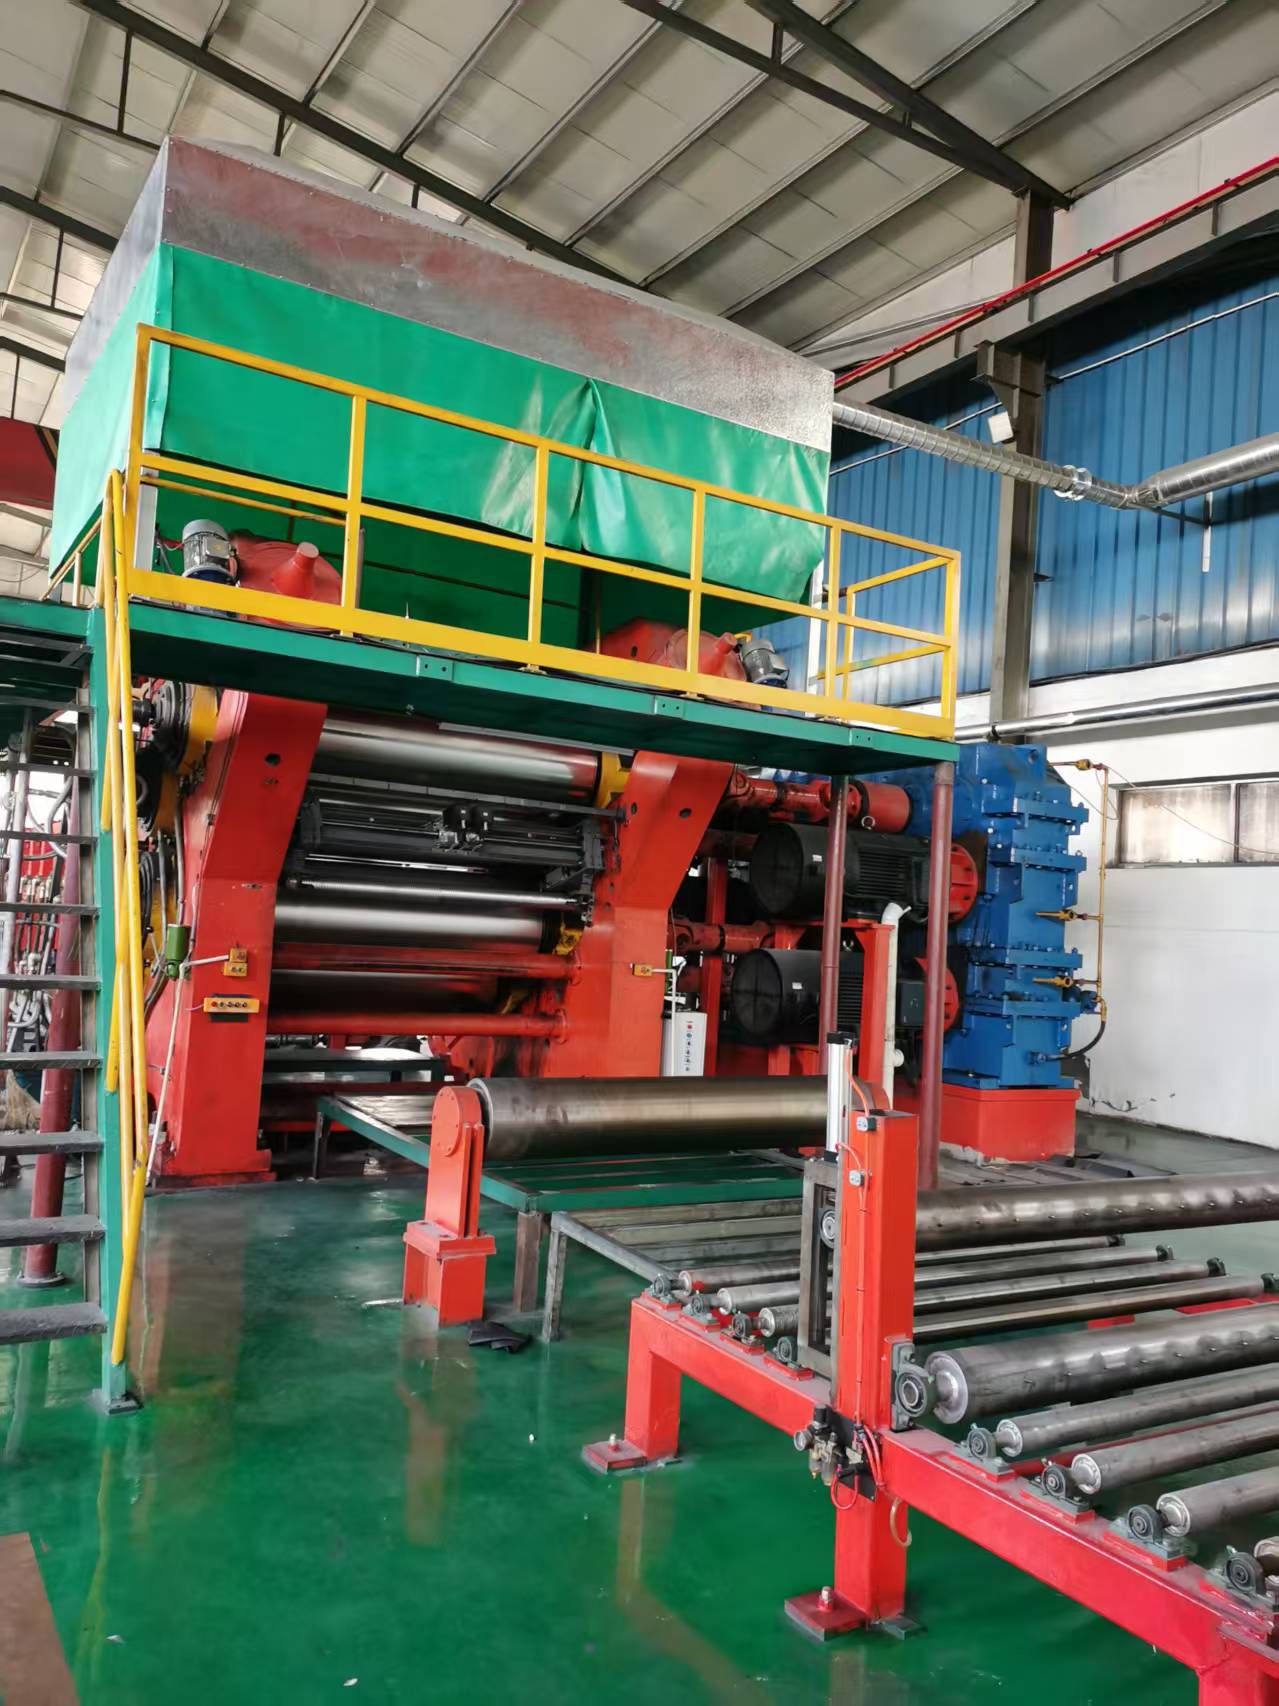
Automated Mixing & Compounding
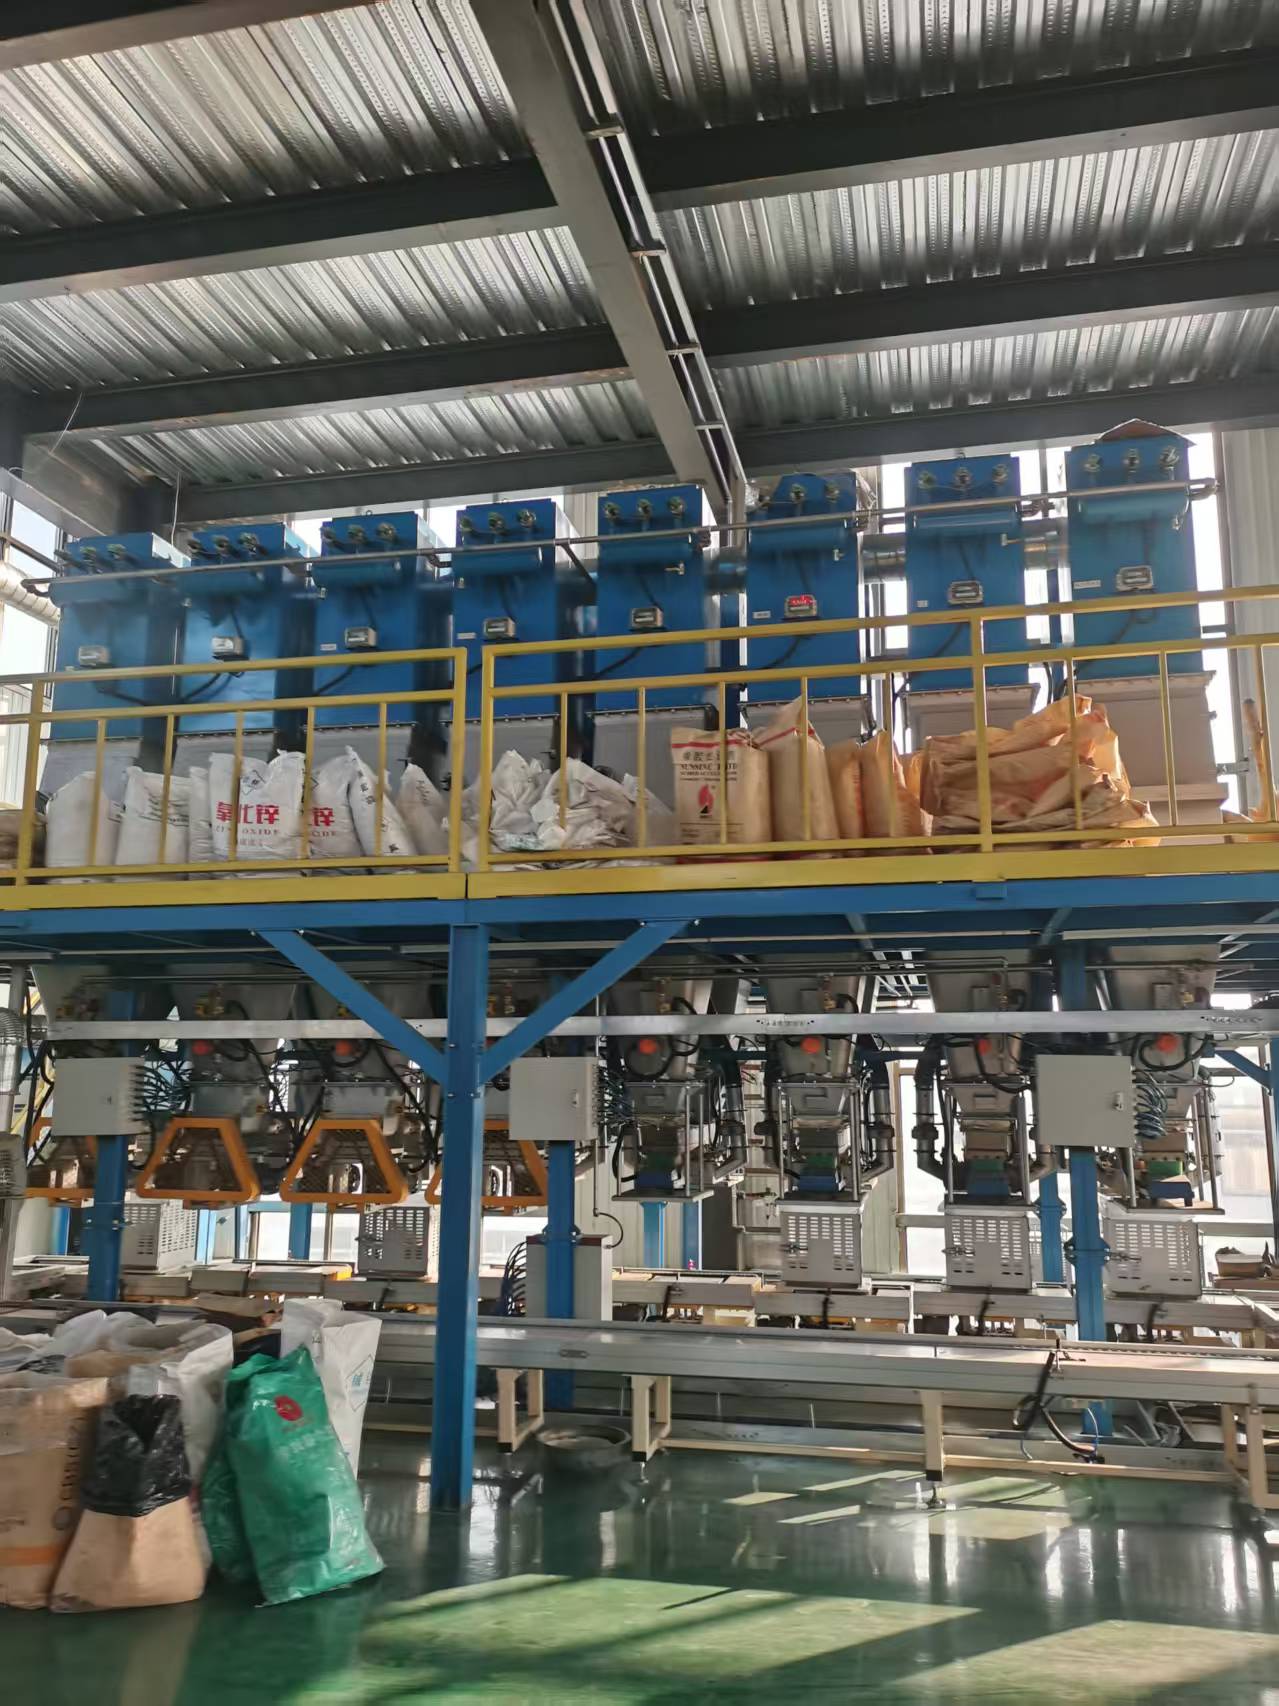
High-Capacity Belt Slitting Line
Steel Cord Tensioning Unit
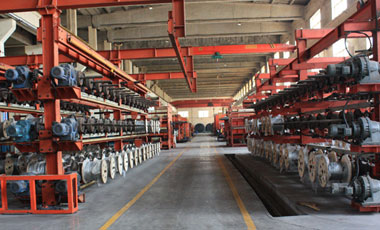
Fabric Ply Laminating Station
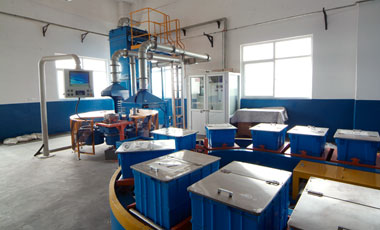
Internal Batch Mixer
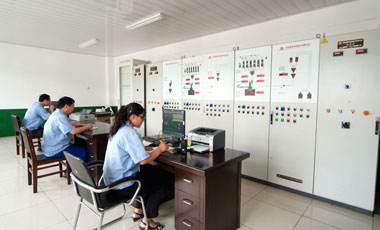
PLC-Controlled Cooling Line
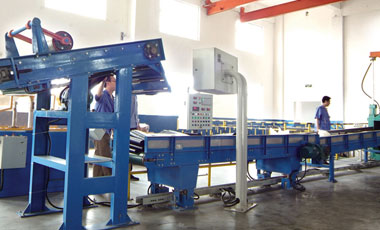
Extrusion Head Assembly
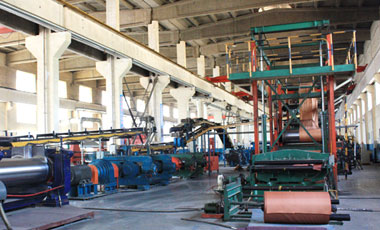
Winding & Packaging Station
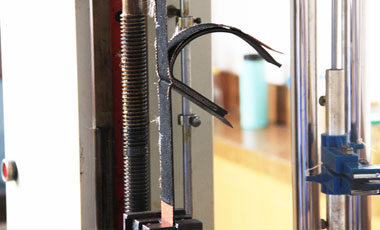
Peeling Test Station
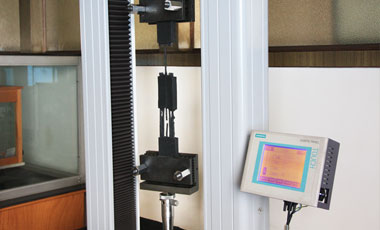
Steel Cord Pull-out Machine
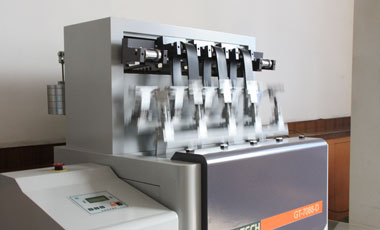
Dynamic Fatigue Tester
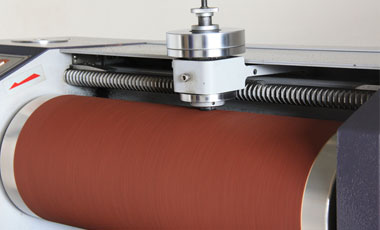
Abrasion Tester (DIN Standard)
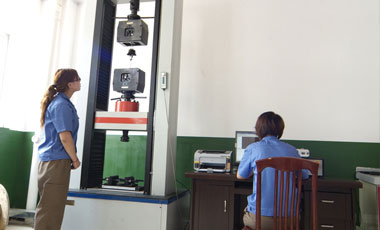
Micro-Abrasion Analysis
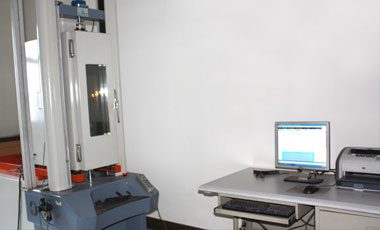
Physical Properties Testing
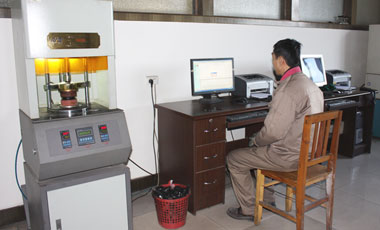
Tensile Strength & Elongation Test
How we are adapting our technology to align with global standards and San Francisco's local progressive policies.
With environmental conservation at the forefront of Northern California's agenda, we are continuously researching bio-based rubber compounds and recyclable thermoplastic elastomers. Our factory is progressively substituting petroleum-based process oils with renewable plant-derived oils, significantly reducing the carbon footprint of our manufacturing process without sacrificing the mechanical integrity of the conveyor belts.
Wildfire risks and strict urban building codes in California have mandated the use of premium-grade flame-retardant materials. Our Flame Retardant Rubber Conveyor Belts comply with stringent international safety protocols, ensuring that in the event of an electrical failure or friction-induced heat, the belt self-extinguishes, protecting vital infrastructure in enclosed spaces like tunnels and processing plants.
In high-throughput sectors like aggregate processing and bulk cargo shipping in San Francisco, belt wear is a major operational expense. By utilizing state-of-the-art carbon black reinforcement and premium synthetic polymers, we produce belts with incredibly low abrasion loss (measured in cubic millimeters under DIN standards). This translates to twice the operational lifespan compared to standard off-the-shelf conveyor belts.
Our Heat-Resistant and Cold-Resistant belts are engineered to perform in extreme microclimates. Whether handling scorching foundry materials or operating in cold storage logistics hubs near SFO, our specialized compound formulas prevent cracking, hardening, or premature aging, securing a seamless supply chain flow.
Providing San Francisco businesses with custom dimensions, robust ply configurations, and world-class physical properties.
Every single belt is subjected to rigorous testing protocols to ensure maximum longevity and performance safety.
Our modern laboratory conducts extensive testing on every batch of raw rubber compound before it enters the calendaring stage. We test for tensile strength, elongation at break, and hardness (Shore A). For our clients in the Bay Area handling abrasive materials like crushed granite, concrete, or glass cullet, we verify the wear resistance of our compounds using DIN abrasion testers, ensuring our products exceed industry averages.
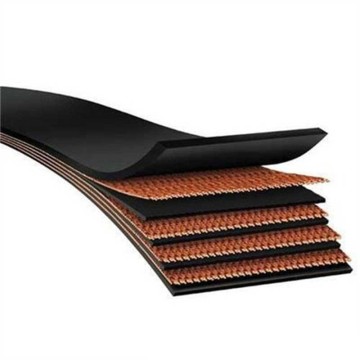
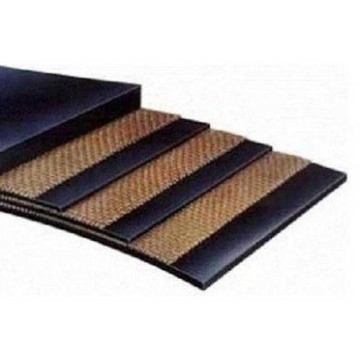
Additionally, we measure the adhesion strength between the rubber covers and the inner fabric or steel cord reinforcements. High adhesion prevents delamination, which is the leading cause of premature conveyor belt failure under heavy loads.
We understand that no two conveyor systems are exactly alike. That is why we offer comprehensive technical support and custom fabrication services for businesses across San Francisco. Whether you require specific cleat profiles, corrugated sidewalls, or precise mechanical fastener preparations, our team of experienced engineers is ready to assist you.
By analyzing your conveyor's pulley diameters, belt speeds, load characteristics, and environmental conditions, we formulate the exact rubber compound and carcass construction to optimize your system's performance and minimize operational costs.